How Accurate Is an AAC Batching System?
How accurately an AAC batching system measures raw materials can directly influence block consistency, production efficiency, and operating costs. But accuracy depends on more than the batching equipment alone: material preparation, moisture control, weighing devices, and calibration all play a role. For manufacturers evaluating AAC sand grinding equipment cost alongside a complete production line, understanding these factors is essential to making an informed investment. This article explores what affects batching accuracy and how to maintain reliable performance.
What does batching accuracy mean in an AAC plant?
An autoclaved aerated concrete (AAC) batching system measures ingredients such as sand slurry, cement, lime, gypsum, water, and aluminum-based expanding agent before they enter the mixer. The exact recipe and material-handling arrangement vary by plant. Some facilities use fly ash or other suitable siliceous materials in place of part or all of the sand.
Accuracy is the closeness of the actual delivered quantity to the recipe target. Repeatability is the ability to deliver a similar quantity from batch to batch. Both matter. A system that consistently adds too much water may be repeatable without being accurate; one that averages the correct quantity but varies widely between batches can also cause production problems.
There is no single accuracy figure that describes every AAC batching system. Performance depends on the ingredient, batch size, weighing range, material behavior, and measurement method. A supplier’s stated tolerance is useful only when its basis is clear: is it a percentage of the target quantity, the scale’s full capacity, or a laboratory test value for the load cell alone?
For example, a tolerance expressed as a percentage of full scale can represent a much larger proportion of a small ingredient dose than of a large one. When comparing proposals, ask for the expected delivered-batch tolerance for each material at the smallest and largest operating batch sizes—not just a general figure for the weighing system.
A correct weight is not always a correct recipe
Sand slurry is a useful example. The scale can measure the requested slurry weight accurately while the quantity of dry solids in that slurry changes. If the slurry becomes more diluted, the same measured weight delivers less sand and more water. The control system may show that the setpoint was achieved even though the effective recipe has shifted.
That distinction matters because the reaction, rising behavior, green-cake strength, and final properties of AAC depend on the combined recipe and process conditions. Batching error is not the only possible cause of variation, but it can make troubleshooting difficult when operators rely on displayed weights alone.
Consider a plant that adds water directly to the mixer and also receives water through sand slurry and recycled materials. Its recipe calculation needs to account for all relevant water streams. Otherwise, an adjustment made at the water scale may compensate for an unnoticed change elsewhere, leaving operators uncertain about the real cause of inconsistent casting behavior.
The role of slurry density and mixing
A representative slurry density measurement helps convert a wet slurry quantity into an estimate of solids and water. Its usefulness depends on how and where the sample is taken. Settling in a storage tank, inconsistent agitation, or a measurement point that does not represent the material entering the batch can all undermine the calculation.
Ask how the proposed plant will keep slurry homogeneous during normal operation and stoppages. Also establish who will check density, how often checks will be made, and whether recipe corrections are automatic or operator-entered. An automated correction is only as dependable as the measurement and assumptions behind it.
Where batching errors usually enter the process
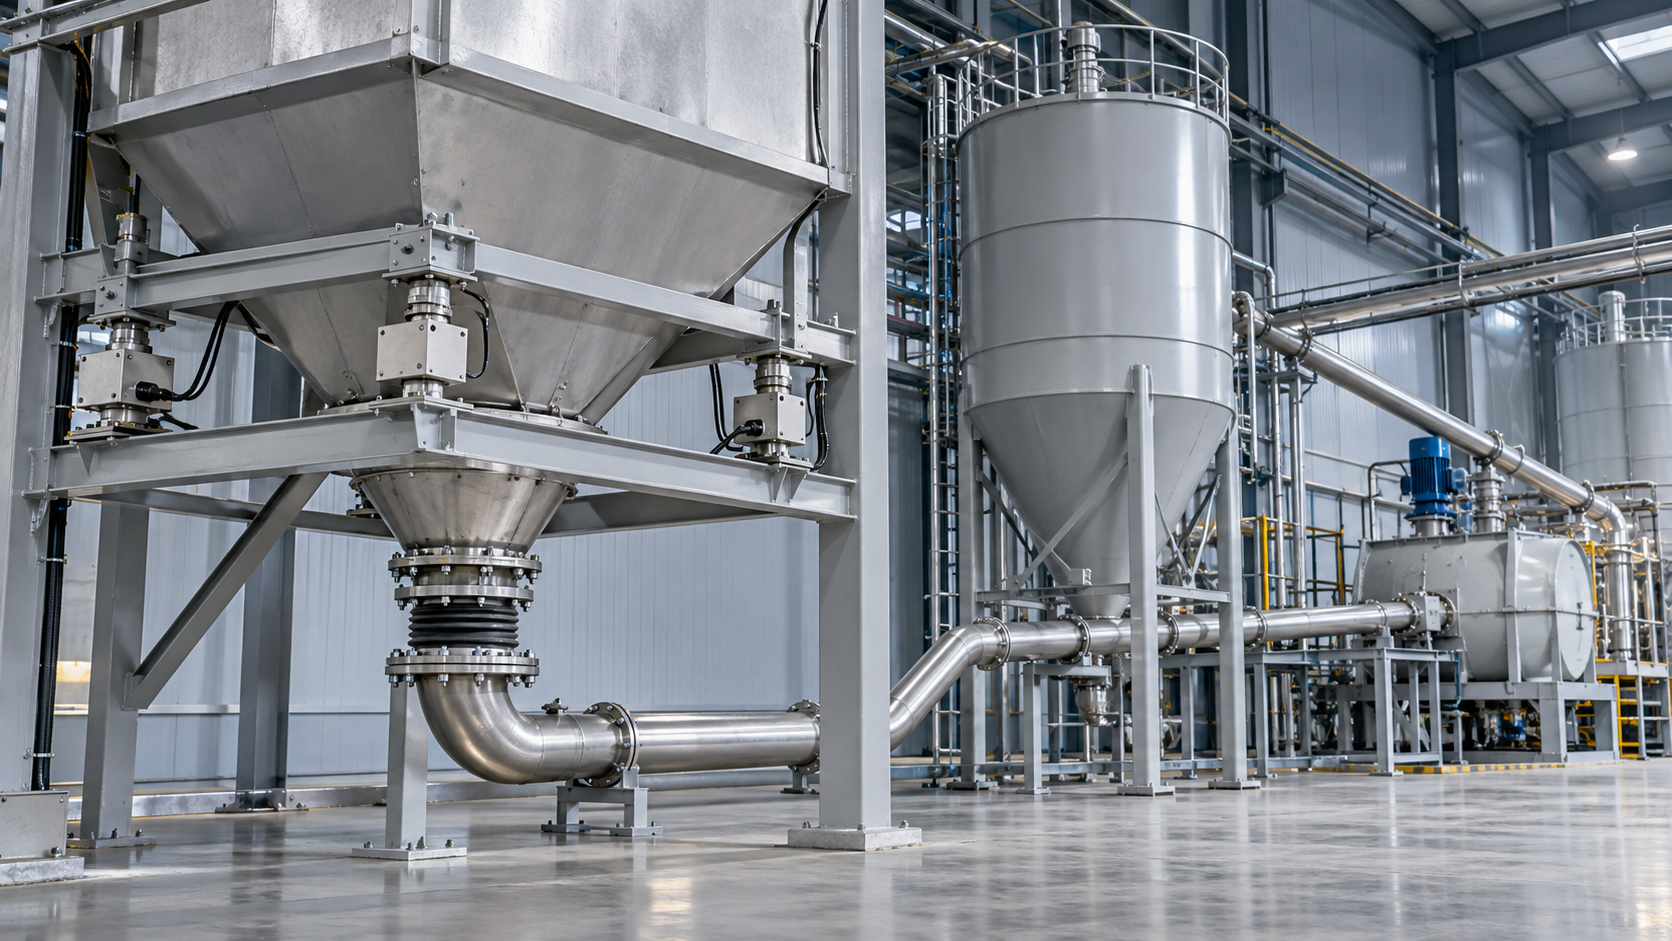
The weighing device is only one part of the dosing chain. Material has to flow into the weighing vessel, stop at the right moment, and then reach the mixer without an unknown quantity being retained or added later. Several practical issues deserve attention during design and commissioning.
- Material in flight: Powder or slurry may continue moving after a feeder or valve receives its stop command. Controls can compensate for this, but the correction needs to match actual flow behavior.
- Variable discharge: Powder bridging, buildup, inconsistent feeder speed, or a partially obstructed valve can make the delivered dose less predictable.
- Mechanical interference: A weighing hopper can give misleading readings if pipes, cables, rigid connections, or accumulated material restrict its movement.
- Scale selection: A scale sized for a large main ingredient may not resolve a small additive dose adequately. Separate dosing equipment may be needed for materials used in small quantities.
- Transfer losses: Material left in a hopper, screw conveyor, chute, or pipe means the quantity weighed is not necessarily the quantity delivered to the mixer.
Environmental conditions can also interfere. Vibration from nearby equipment, unstable supports, and electrical or signal problems may affect readings. Good design reduces these influences; commissioning checks should confirm that the installation behaves as intended.
How sand grinding affects the batching system
Grinding does not directly determine the accuracy of a load cell. It does, however, influence the material that arrives at the slurry preparation and batching stages. Changes in sand feed, grinding performance, water addition, and slurry storage can change the consistency of the material being dosed.
Fineness is also a process variable in its own right. If the particle characteristics of the sand slurry change, the plant may need to review its recipe or process settings even when the measured slurry weight remains stable. The required fineness should be established through the selected raw materials, product targets, and process design rather than assumed from a generic equipment specification.
This is why AAC sand grinding equipment cost should be evaluated beyond the purchase price of the mill. A meaningful comparison also considers the equipment and operating work needed to produce a consistent feed for batching. Depending on the project, that may include material conveying, water supply and measurement, slurry tanks, agitation, pumping, instrumentation, and maintenance access.
A lower equipment quotation can be misleading if essential tanks, pumps, controls, installation work, or wear parts are excluded. Conversely, a more elaborate arrangement is not automatically justified for every plant. The sensible choice depends on raw-material variation, production capacity, the degree of automation required, and how the grinding section connects to the rest of the line.
How to verify accuracy before accepting a line
An acceptance test should distinguish a scale calibration from a complete dosing test. Calibration checks the weighing instrument against suitable reference weights or another agreed method. A dosing test examines what the system actually delivers under defined operating conditions. Both are valuable, but they answer different questions.
Agree on the test procedure before installation is complete. For each ingredient, the procedure should identify the target dose, permitted deviation, measurement method, number of runs, material condition, and operating range. If slurry is involved, specify whether the test assesses wet weight only or also checks the solids basis used for the recipe.
Where practical, test at more than one batch size and include a sequence representative of normal operation. A result obtained with a clean, empty hopper and a single carefully supervised dose may not reveal buildup, settling, or variations that develop over repeated batches. Record individual results rather than relying only on an average.
The agreed acceptance criteria should also state how to handle a result outside tolerance: whether the supplier will adjust controls, inspect the mechanical installation, repeat the test, or investigate the raw material. This avoids an argument later over whether a problem belongs to the weighing system or to upstream preparation.
Keeping measurements reliable after commissioning
Accuracy is not a one-time setting. Feeders wear, material accumulates, valves change their closing behavior, and maintenance work can disturb weighing connections. A routine inspection and calibration plan should reflect the equipment supplier’s instructions, site conditions, and applicable local requirements.
Operators should be able to check the scale’s zero reading, identify unexpected dosing corrections, and report abnormal filling times. Maintenance staff need access to load cells, flexible connections, valves, and feeder components without having to dismantle unrelated equipment. A system that is difficult to inspect is more likely to develop a small, persistent error that goes unnoticed.
Batch records can help separate random variation from drift. Useful records include recipe setpoints, actual measured doses, alarm events, and relevant slurry measurements. They do not replace physical checks: a control screen can record the same incorrect value repeatedly if the measurement or material transfer is compromised.
Recipe changes deserve the same discipline. When a sand source changes or reclaimed material is introduced, document what changed and reassess slurry behavior and water accounting. Otherwise, operators may repeatedly adjust the mix without resolving the underlying measurement issue.
Making a better equipment comparison
For a new AAC line, batching accuracy should be discussed alongside capacity, raw-material preparation, and operating flexibility. Provide suppliers with the proposed materials, expected batch-size range, target products, available utilities, and any planned use of recycled process material. Ask them to identify assumptions that still need material tests or engineering confirmation.
Shandong Hongfa Scientific Industrial & Trading Co., Ltd., founded in 1990, manufactures construction machinery, including AAC production lines and concrete batching plants. For a project involving both grinding and batching, a line-level discussion can help clarify equipment interfaces: which party supplies the slurry handling, where measurement takes place, and how controls exchange recipe data.
Before comparing final quotations, request a clear equipment scope, dosing tolerances stated on the same basis, a commissioning and acceptance procedure, and a list of recommended maintenance items. Those details make the quoted accuracy—and the cost of achieving it in daily production—much easier to judge.
Recommend
 Nov 09, 2026
What Are the Import Requirements for Construction Machinery?
Understand building machinery import requirements, from customs documents and duties to safety compliance and installation, before you ship.
- Nov 09, 2026
How Accurate Is an AAC Batching System?
Compare AAC sand grinding equipment cost and learn what affects batching accuracy, from slurry control to calibration, before investing in your production line.
- Nov 08, 2026
How Much Does AAC Block Packaging Equipment Cost?
AAC batching system accuracy can affect downstream packaging. Explore AAC block packaging equipment costs, key price factors, and tips for comparing quotes.