Is Shandong Hongfa a Reliable AAC Plant Supplier?
Shandong Hongfa’s reliability as an AAC plant supplier remains unconfirmed without project-specific evidence. A dependable assessment requires proof that the proposed line can process the intended raw materials, sustain the agreed saleable output, and receive effective support after commissioning. Equipment specifications and a quotation establish what is being offered; operating references, engineering documents, and measurable acceptance terms establish how much confidence that offer deserves.
The strongest basis for a positive judgment is a consistent connection between the proposed design, comparable operating installations, and contractual performance commitments. Missing evidence in any of these areas leaves an important part of the investment unresolved.
Start with evidence from a comparable operating plant
A reference installation is useful when its production conditions resemble those of the proposed project. An AAC line processing predominantly sand-based material does not automatically demonstrate competence with a variable fly ash supply. Differences in feedstock chemistry, grinding requirements, product density, and block dimensions affect process settings and equipment loading.
A meaningful reference discussion should establish what material the plant uses, which products it regularly makes, and whether its production records distinguish gross output from accepted finished blocks. It should also clarify how long the installation has operated beyond initial commissioning. A successful demonstration run offers less evidence of sustained reliability than production records covering repeated batches, routine maintenance, and normal changes in material supply.
During a site visit, follow the material through the process. Observe whether slurry preparation remains consistent, whether green cakes reach cutting strength predictably, and whether finished blocks show recurring edge damage or dimensional variation. Frequent manual corrections deserve explanation because they can indicate unresolved process variation, equipment limitations, or incomplete operating procedures.
Reference access also needs to reflect the proposed scope. An installation where another contractor designed the process or supplied major equipment offers limited evidence of the supplier’s ability to deliver the complete package under consideration.
Raw-material compatibility determines whether the design is credible
AAC production connects raw-material preparation, dosing, mixing, rising, cutting, and autoclaving. Errors introduced early in this sequence often appear much later as rejected blocks, making the original cause difficult to isolate. A credible proposal therefore begins with representative material testing and a documented process basis.
Sand fineness and mineral composition affect reaction behavior and preparation requirements. Fly ash introduces a different set of variables, including fineness, unburned carbon, and chemical consistency. Lime reactivity influences heat development and rising behavior, while the suitability of aluminum powder or paste depends partly on its reaction characteristics within the selected mix.
A laboratory result from one convenient sample cannot establish the variability of a long-term supply. Samples should represent the intended sources and realistic changes in material quality. The resulting process proposal should identify the acceptable material range and explain what adjustments are required when feedstock approaches its limits.
Useful engineering evidence includes a material testing report, a proposed formulation basis, slurry preparation requirements, and trial results connecting the mix to the intended product properties. If testing has not yet occurred, the quotation should identify which design assumptions remain provisional and when they must be resolved.
Responsibility for formulation adjustments also matters. A mechanically complete line can still struggle if no party is accountable for adapting the process to local materials during commissioning. That responsibility needs a defined scope, including sampling, trial batches, process adjustments, and documentation of the final settings.
Read capacity claims through the production bottleneck
A headline capacity figure is incomplete unless it states the product mix, density range, operating schedule, and basis of calculation. Mold volume, theoretical daily production, and saleable finished output measure different things. Their relationship changes with cutting losses, rejected batches, maintenance, and the time available for production.
The useful commitment is sustained saleable output under defined conditions. That commitment should connect the capacity calculation to the actual equipment configuration.
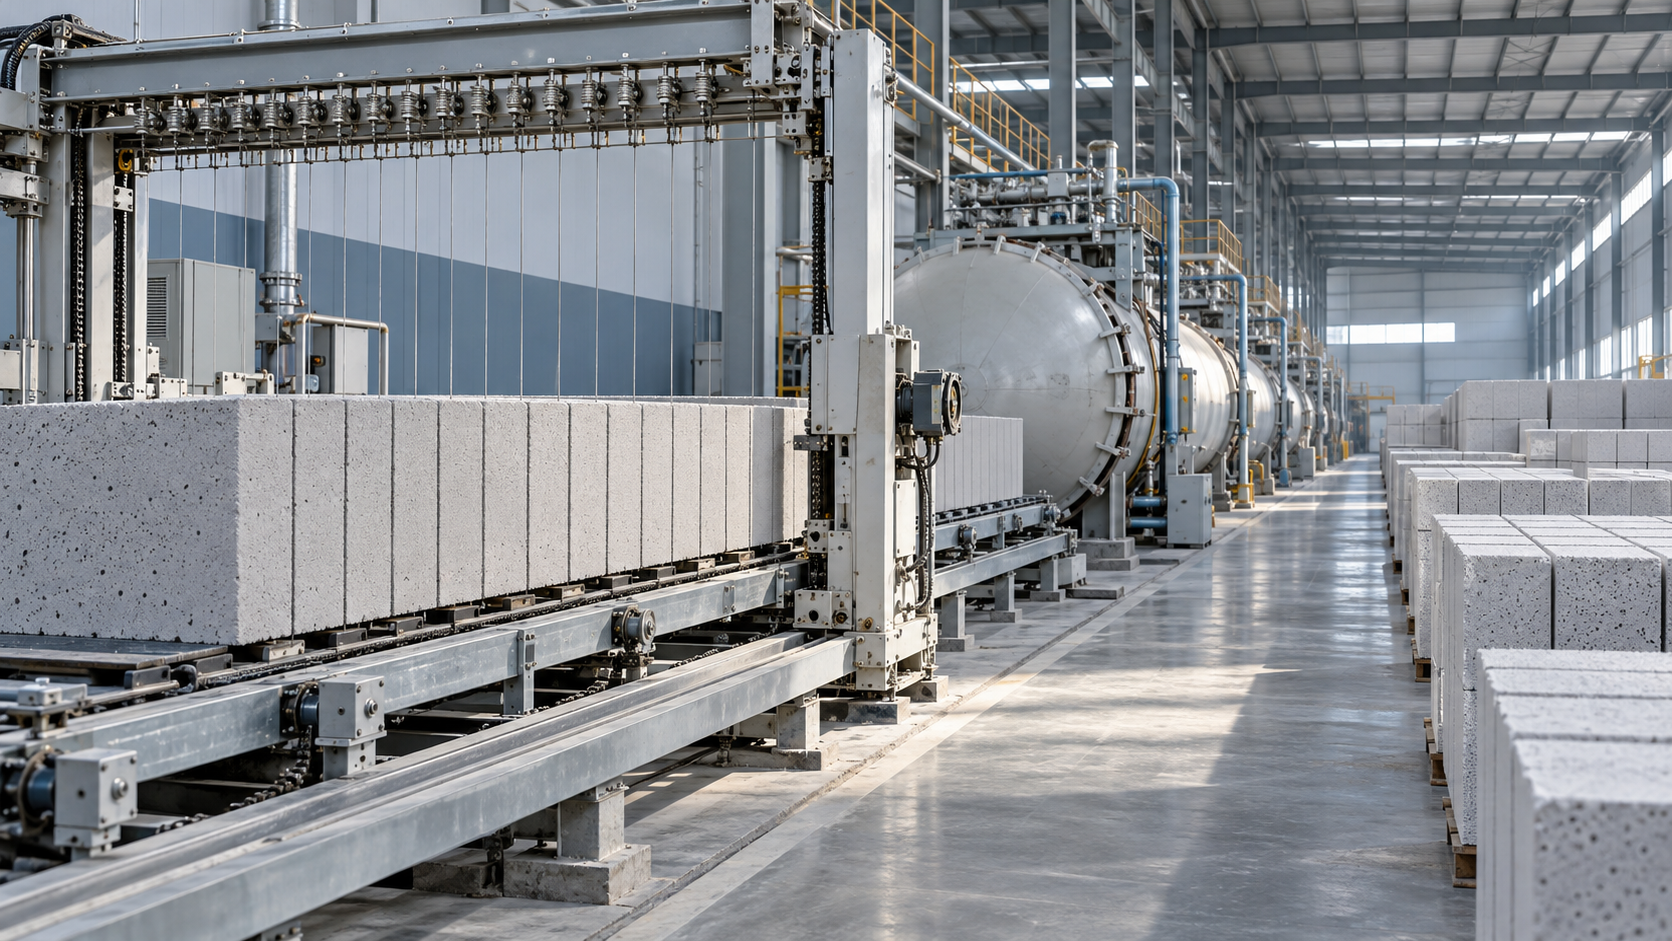
Autoclaves deserve particular attention because their batch cycles must fit the rest of the line. Increasing mixing or casting capacity does little if cakes accumulate while curing equipment remains occupied. Conversely, additional autoclave volume will not resolve a bottleneck caused by inconsistent pre-curing or slow handling.
The production schedule should also show what happens during routine stoppages. Limited buffer space between process stages can turn a local interruption into a wider production loss. A layout drawing becomes more informative when it is supported by a realistic flow and timing calculation.
Equipment quality must be visible in manufacturing records
A factory visit provides stronger evidence when it examines equipment intended for the project or comparable machines under construction. Finished paintwork reveals little about alignment, fabrication consistency, component selection, or inspection discipline.
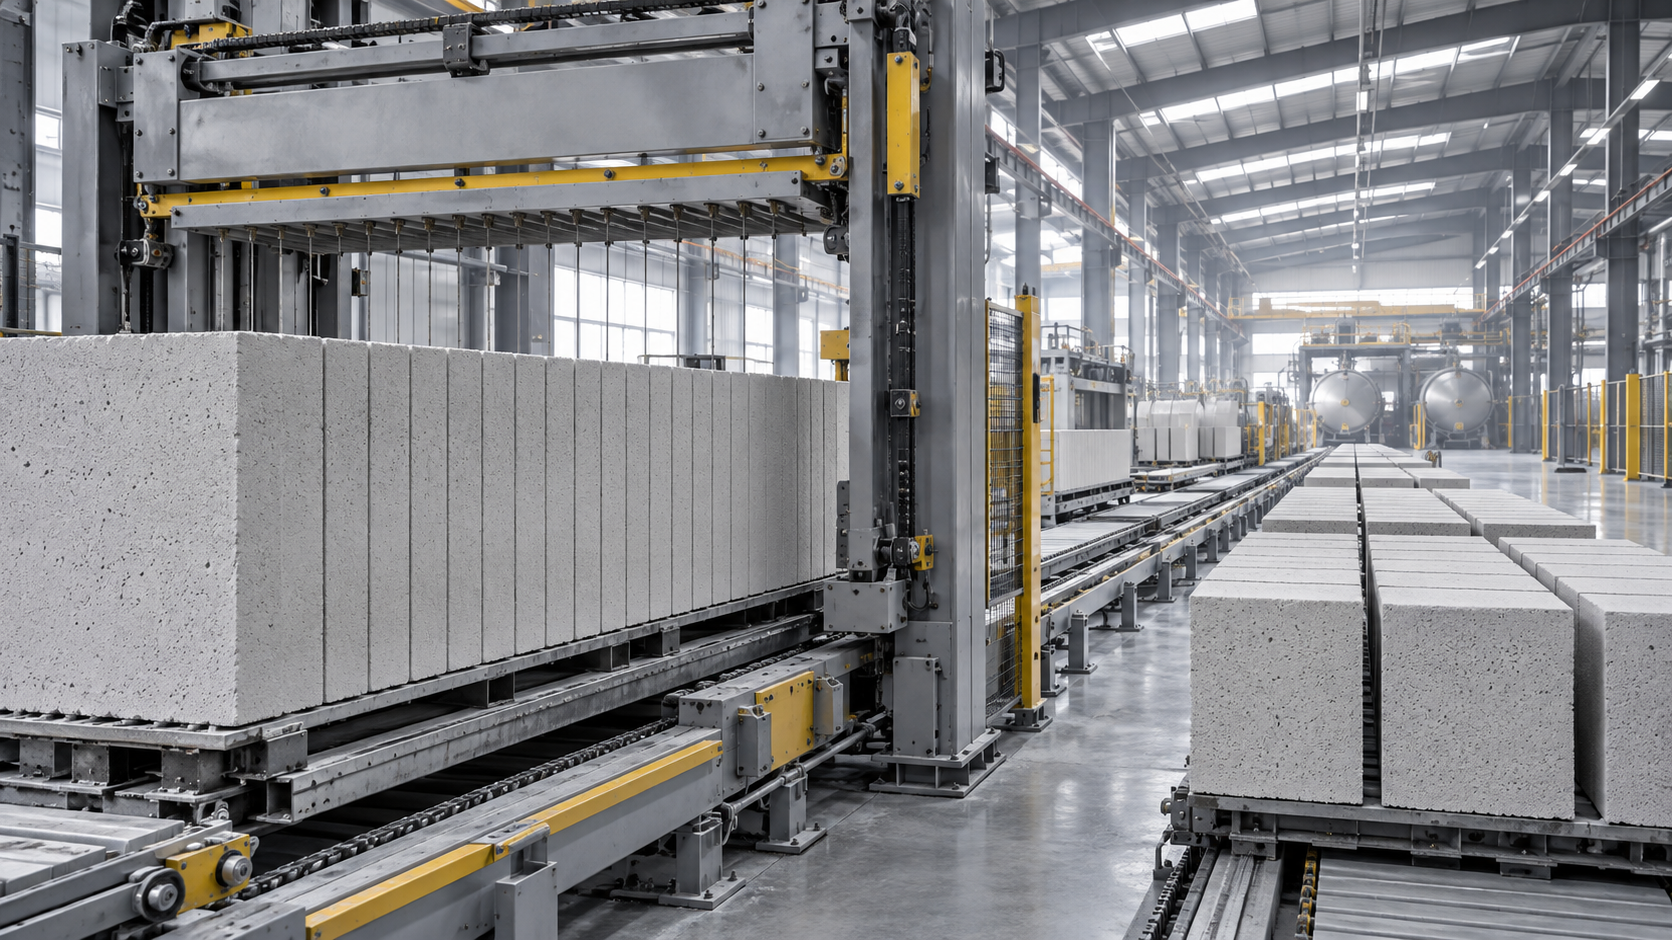
For cutting equipment, relevant details include frame rigidity, guidance arrangements, wire tension control, and access for adjustment. Dimensional accuracy depends on both mechanical condition and the strength of the green cake at cutting. An accuracy promise without a defined process condition leaves the cause of future deviations open to dispute.
Mixing and dosing equipment should support repeatable batches. Weighing arrangements, calibration procedures, slurry agitation, and cleaning access all affect consistency. Residue buildup or unstable slurry concentration can disrupt a process even when the nominal weighing accuracy appears satisfactory.
Autoclaves require separate scrutiny as pressure equipment. Material traceability, welding records, inspection documentation, door interlocks, and the applicable approval route must be established for the installation location. A general quality-management certificate does not establish that an individual pressure vessel meets those requirements.
Purchased components should be identified precisely enough to support maintenance. Motor, gearbox, bearing, valve, sensor, and control-system specifications affect replacement availability. Where substitutions are permitted, the approval procedure should preserve the agreed performance and compatibility.
Commissioning should prove a repeatable process
Mechanical installation and first production are distinct milestones. A line that produces acceptable blocks during a closely supervised trial has demonstrated initial capability. Reliable handover requires evidence that acceptable production can be repeated using documented settings and routine operating procedures.
The acceptance agreement should define the products to be made, the raw materials to be used, the required output, and the test conditions. It should also identify how dimensions, dry density, compressive strength, and visible defects will be assessed. Density and strength need to be considered together because changing density alters the basis on which strength performance is judged.
Moisture condition and sample preparation affect test results. The contract should name the agreed test method and sampling procedure, including how samples represent the production run. Without these details, apparently conflicting results can arise from different testing practices.
A practical acceptance arrangement addresses several connected points:
- Run duration and continuity: the demonstration period must be long enough to expose recurring process or equipment interruptions.
- Saleable output needs a clear definition, including treatment of broken blocks, dimensional rejects, and material requiring reprocessing.
- Utility conditions should be recorded. Steam supply, electrical capacity, water availability, and compressed air must match the agreed design basis.
- If performance falls short, the agreement should identify the correction process, responsibility for repeat testing, and the conditions for final acceptance.
Commissioning records should preserve the settings that produced acceptable results. Batch formulations, slurry conditions, rising observations, cutting timing, and autoclave schedules provide a starting point for troubleshooting after handover. Training has greater value when it uses these records and addresses actual deviations observed during startup.
Installation boundaries and support commitments expose hidden gaps
An AAC plant quotation can appear complete while leaving important interfaces outside its scope. Foundations, embedded parts, steam generation, water treatment, electrical distribution, and installation equipment all require clearly assigned responsibility. An omitted interface can delay commissioning even when every supplied machine arrives on time.
Foundation and layout drawings should include the loads, elevations, access clearances, and connection points needed for local engineering. Steam requirements need to be defined at the equipment interface, including pressure, quality, and demand over the operating cycle. A boiler selected solely around an average consumption figure can struggle with simultaneous peak demand.
Support quality is best assessed through a specific service arrangement. Remote assistance requires usable alarm records, accessible drawings, and an agreed method for reviewing process data. On-site support requires defined mobilization arrangements and responsibility for travel and related costs. Broad promises of continuous service leave these practical issues unanswered.
Spare-parts planning should distinguish routine wear from failures that stop production. Cutting wires and seals require predictable replenishment. A failed drive, control module, or specialized valve can create a longer interruption if identification and replacement arrangements are unclear. Parts lists should include specifications, drawings where appropriate, and realistic availability information.
Control-system access also affects maintainability. Handover should address program backups, parameter records, software licensing, and the access needed to diagnose faults or replace hardware. These details determine how effectively the plant can recover from failures throughout its operating life.
What would justify a positive decision?
A positive assessment of the proposed supplier is justified when comparable references, raw-material trials, equipment records, and contractual commitments support the same operating outcome. Unresolved assumptions should remain visible in the technical agreement, with responsibility and completion dates attached.
The decision should remain open if the offer relies on nominal capacity, unspecified major components, or acceptance terms that leave product quality and output undefined. A technically credible proposal gives each important promise a measurable basis and an identifiable record through which performance can be confirmed.
Recommend
 Oct 29, 2026
What Export Experience Does Shandong Hongfa Building Machinery Have?
Assess Shandong Hongfa building machinery export experience through project records, delivery planning, and after-sales support. Discover what to verify before your next equipment purchase.
- Oct 29, 2026
What Do Reviews Say About Hongfa AAC Block Production Lines?
Hongfa AAC block production line reviews: Learn how to verify output, block quality, energy use, and service support before investing. Discover the evidence buyers should request.
- Oct 29, 2026
Is Shandong Hongfa a Reliable AAC Plant Supplier?
Is Shandong Hongfa a reliable AAC plant supplier? Explore key checks on operating references, raw materials, output guarantees, and support before making your investment decision.