‹
›
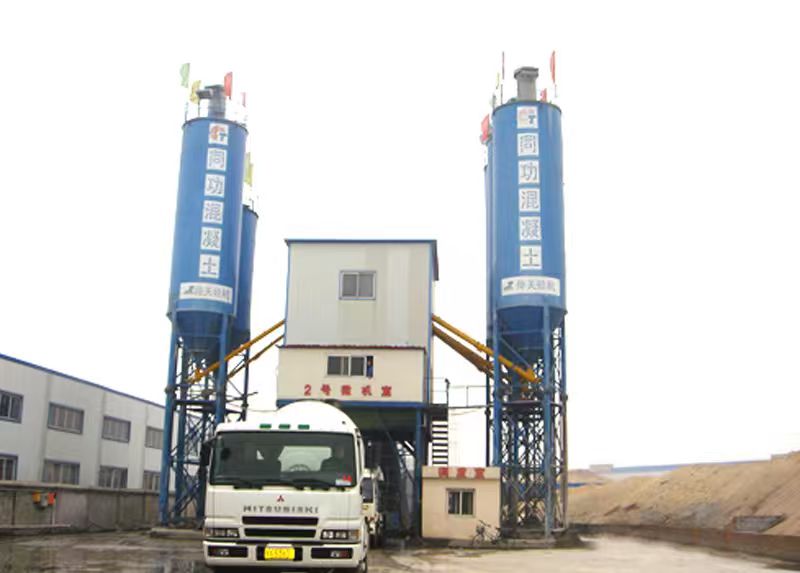
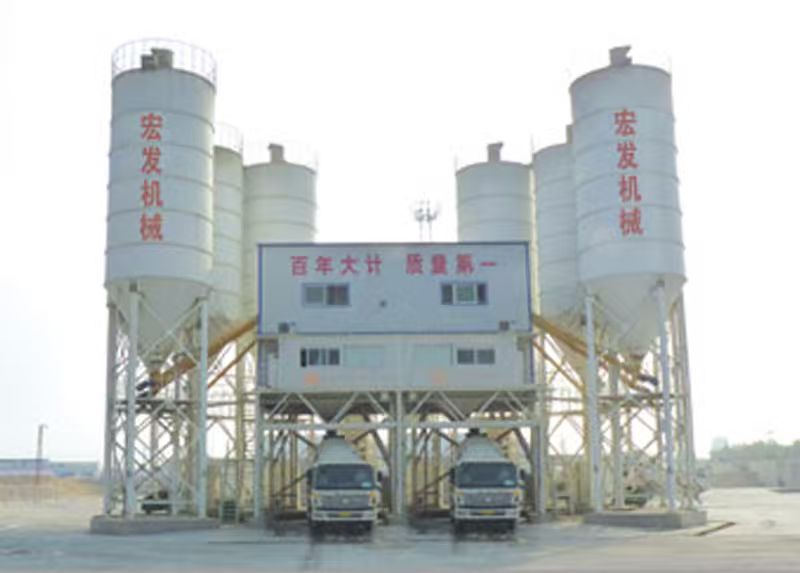
HZS60 Concrete Mixing Plant (60 m³/h)
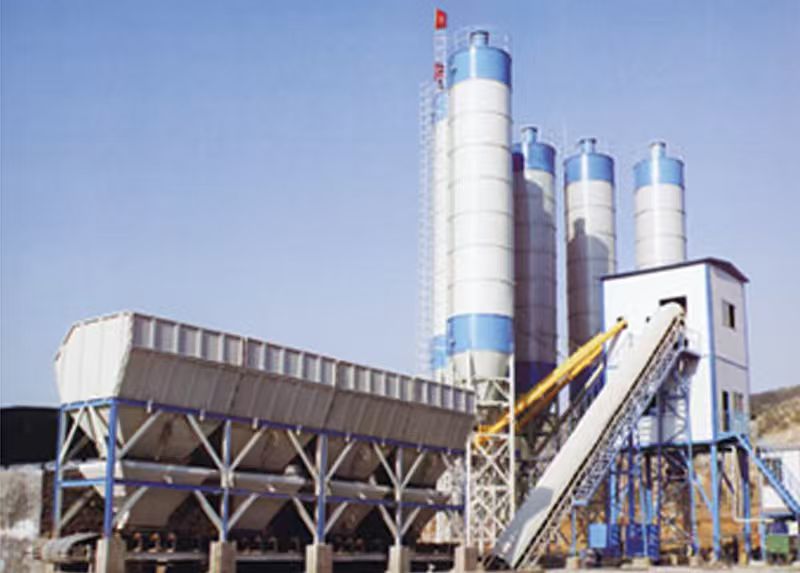
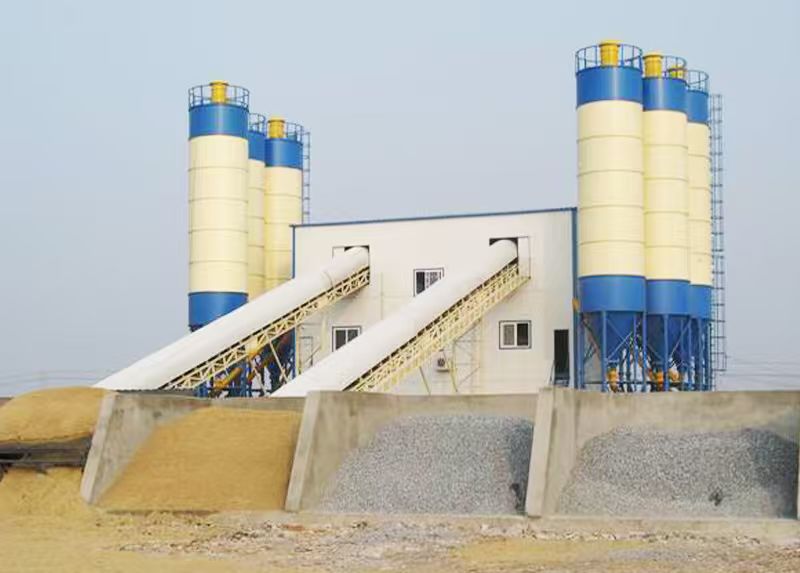
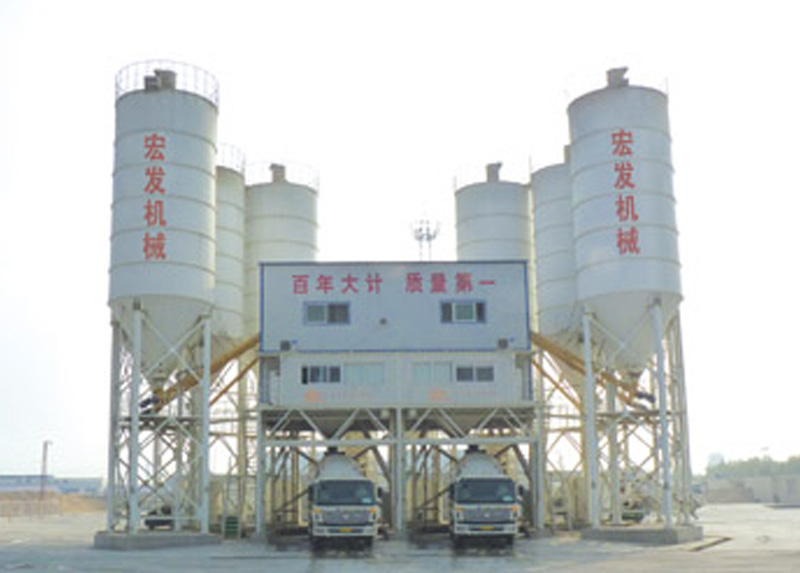
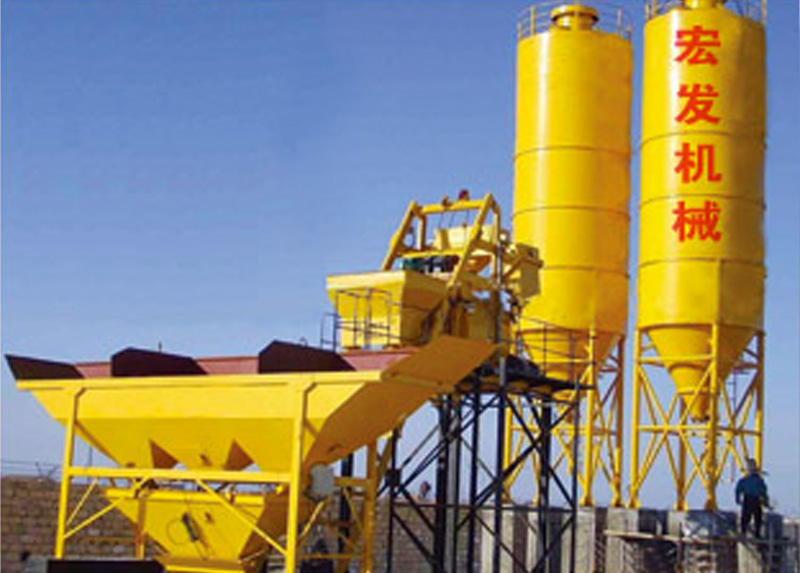
The HZS60 Concrete Mixing Plant is a modular, fully automated batching station with a theoretical production capacity of 60 cubic meters per hour. Engineered for high efficiency, it features a compulsory twin-shaft mixer and a precise weighing system to ensure consistent product quality. Its compact, skid-mounted design significantly reduces the required installation footprint, making it ideal for medium-sized construction projects, bridges, and precast concrete factories. The plant is equipped with a centralized industrial computer control system, allowing for simplified operation and convenient maintenance. With its reliable performance and low operational costs, the HZS60 provides a highly cost-effective and durable solution for continuous concrete production.
All PRODUCTS
Stay Connected
If you have any questions, please contact us and we will contact you as soon as possible.
Prduct Introdution
HZS60 Concrete Mixing Plant
1. Product Overview
The HZS60 integrates aggregate batching, material weighing, conveying, mixing, and centralized control into one coordinated production system.
The plant uses a twin-shaft compulsory mixer to thoroughly mix aggregates, cement, water, and additives. Each material is accurately weighed before entering the mixer, helping maintain consistent mix proportions and stable concrete quality.
With automated control and a modular structure, the HZS60 provides a practical balance between production capacity, installation efficiency, operational convenience, and investment cost.
2. Main Features
60 m³/h Theoretical Production Capacity
The HZS60 is designed with a theoretical production capacity of 60 cubic meters of concrete per hour, making it suitable for medium-scale continuous concrete production.
Actual output may vary depending on material characteristics, concrete mix design, loading efficiency, plant configuration, and operating conditions.
Twin-Shaft Compulsory Mixer
The plant is equipped with a twin-shaft compulsory mixer that provides strong and efficient mixing action.
The twin-shaft system helps achieve:
Thorough material blending
Uniform concrete consistency
Efficient mixing cycles
Stable production quality
Adaptability to different concrete mix designs
Precision Weighing System
Accurate weighing is essential for maintaining consistent concrete quality.
The HZS60 uses an independent weighing system for the main materials, helping control the proportion of:
Aggregates
Cement
Water
Admixtures
Other optional materials
Precise batching helps reduce material variation and supports repeatable concrete performance.
3. Fully Automated Control System
The HZS60 adopts a centralized industrial computer control system for automated plant operation.
The control system coordinates key production processes, including:
Aggregate batching
Material weighing
Conveyor operation
Mixing
Discharge
Production monitoring
Operators can monitor and manage production from a centralized control station, reducing manual intervention and simplifying daily operation.
4. Modular and Compact Design
The HZS60 features a modular skid-mounted structure, which helps simplify equipment installation, transportation, and site organization.
Compared with more complex fixed plant layouts, the compact design can reduce the required installation footprint while maintaining the required production functions.
This makes the HZS60 particularly suitable for projects where site space is limited.
5. Efficient Concrete Production Process
The basic production workflow is:
Aggregate Storage → Automatic Batching → Precision Weighing → Material Conveying → Twin-Shaft Mixing → Concrete Discharge → Delivery
The integrated system helps keep the production process organized and continuous, reducing unnecessary material handling and improving overall productivity.
6. Applications
The HZS60 Concrete Mixing Plant is suitable for a wide range of applications, including:
Medium-Sized Construction Projects
Provides continuous concrete supply for building foundations, structural components, and general construction.
Bridge and Infrastructure Projects
Suitable for road, bridge, tunnel, and other infrastructure construction requiring stable concrete production.
Precast Concrete Factories
Provides reliable batching and mixing for precast concrete components and products.
Commercial Construction
Can supply concrete for commercial buildings, industrial facilities, and large-scale building projects.
Municipal Engineering
Suitable for roads, drainage systems, public facilities, and other municipal construction applications.
7. Production Advantages
High Mixing Efficiency
The twin-shaft compulsory mixer provides strong mixing action and efficient material blending, helping shorten mixing cycles while maintaining uniformity.
Stable Concrete Quality
The combination of precision weighing and controlled mixing helps maintain consistent mix proportions and repeatable concrete quality.
Reduced Labor Requirements
Automated batching, weighing, conveying, and mixing reduce the need for manual operation and improve production efficiency.
Convenient Operation
The centralized computer control system makes plant operation and production monitoring more straightforward.
Easy Maintenance
The modular structure and organized equipment layout facilitate inspection, maintenance, and replacement of components.
Lower Operating Costs
The combination of automated operation, efficient mixing, and optimized material handling helps control labor and production costs.
8. Modular Configuration
The HZS60 can be configured according to different project requirements and site conditions.
Optional system configurations may include:
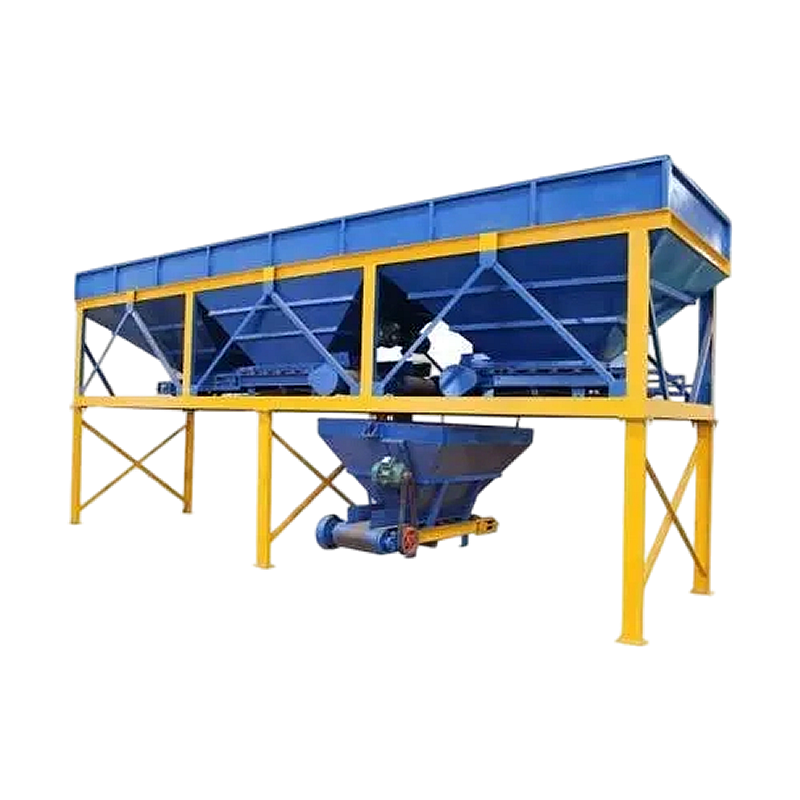
Aggregate storage and batching systems
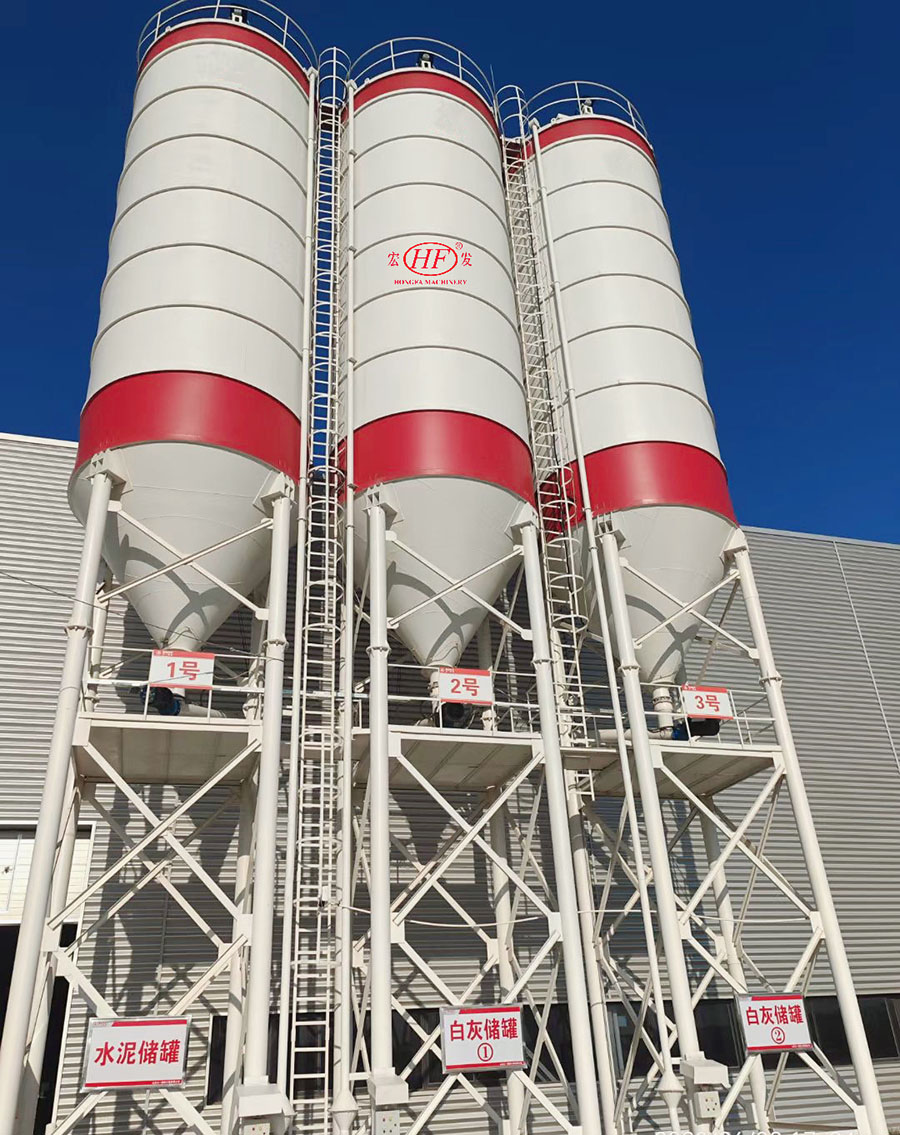
Cement silos
Fly ash silos
Screw conveyors
Water weighing systems
Admixture dosing systems
Control systems
Dust collection equipment
This allows the plant to be adapted to different concrete formulas, site layouts, and production requirements.
9. Quality and Reliability
The HZS60 is designed for continuous industrial operation and emphasizes mechanical stability and process consistency.
Its robust structure and automated control system help provide:
Reliable plant operation
Consistent batching accuracy
Stable mixing performance
Reduced production interruptions
Improved production repeatability
Regular maintenance and correct operation are essential to maintaining long-term equipment performance.
10. Key Advantages
60 m³/h Theoretical Capacity
Suitable for medium-scale continuous concrete production.
Twin-Shaft Compulsory Mixing
Provides strong mixing performance and uniform concrete quality.
Precision Batching and Weighing
Accurately controls material proportions for consistent concrete production.
Fully Automated Control
Centralized computer control simplifies operation and production monitoring.
Compact Skid-Mounted Design
Reduces installation space and simplifies plant layout.
Easy Maintenance
Modular equipment arrangement provides convenient access for inspection and servicing.
Cost-Effective Operation
Designed to balance production capacity, energy consumption, labor requirements, and maintenance costs.
11. Product Summary
The HZS60 Concrete Mixing Plant is a reliable and efficient solution for 60 m³/h-class concrete production. Featuring a twin-shaft compulsory mixer, precision weighing system, centralized industrial computer control, and compact modular structure, it provides stable performance and consistent concrete quality.
Its combination of automation, efficient mixing, compact installation, easy maintenance, and controlled operating costs makes the HZS60 particularly suitable for medium-sized construction projects, bridge and infrastructure works, precast concrete factories, and commercial construction.
For customers seeking a durable and economical concrete batching solution with reliable continuous production capability, the HZS60 provides a practical choice for modern concrete manufacturing.
Previous page: QT4-20C Block Making Machine
Next page: HZS35 Concrete Mixing Plant (30 m³/h)
Inquiry
HOT Products
")
HZS75 Concrete Mixing Plant (75 m³/h)
")
HZS100 Concrete Mixing Plant (100 m³/h)
")
HZS120 Concrete Mixing Plant (120 m³/h)
")
HZS25 Concrete Mixing Plant (25 m³/h)
")
HZS35 Concrete Mixing Plant (30 m³/h)
")
HZS60 Concrete Mixing Plant (60 m³/h)

Ball Mill

Concrete Silo

PLD1200 sand batching machine,batching plant,three hopper batching machine