How Accurate Should AAC Ingredient Dosing Be?
How accurate should AAC ingredient dosing be? The answer depends on the material, mix design, and production process, but consistent measurement is essential to achieving reliable aerated concrete quality. Even small variations in cement, lime, water, or aluminum powder can affect slurry behavior, density, and strength. This guide explores dosing accuracy, the factors that influence it, and how well-designed batching equipment can help AAC manufacturers improve consistency and reduce waste.
The useful answer is ingredient-specific
There is no single dosing tolerance that can responsibly be applied to every autoclaved aerated concrete plant. A workable target must reflect the approved recipe, batch size, material variability and the properties required of the finished blocks or panels. It should also be achievable with the actual equipment throughout its operating range, not just under ideal test conditions.
The practical objective is to keep each ingredient close enough to its intended quantity that normal measurement error does not push the mix outside its acceptable operating window. That window is established through mix trials, production experience and product testing. A plant making a lower-density product may find its process responds differently to variation than a plant making a denser grade with another raw-material combination.
It is also important to distinguish accuracy from repeatability. A feeder that consistently delivers the wrong quantity is repeatable but inaccurate. A calibrated system that produces large batch-to-batch swings is not sufficiently repeatable. AAC production needs both: a measurement close to the target and predictable performance over consecutive batches.
Why the same percentage does not tell the whole story
Dosing error is often expressed as a percentage of the target batch quantity. For example, if the target for an ingredient is 1,000 kg and the actual delivered amount is 1,010 kg, the error is 10 kg, or 1% of the target. That calculation is simple, but the basis matters: a percentage of full scale is not the same as a percentage of the actual dose.
Consider a weighing hopper rated for a large batch but used to measure a much smaller amount. An error that appears small relative to the hopper’s full capacity may represent a significant fraction of the ingredient actually being dosed. This is particularly relevant for small additions such as aluminum, where scale resolution, minimum operating load and residue can matter as much as the rated maximum capacity.
When comparing equipment proposals, ask whether the stated tolerance applies to the indicated weight in the hopper or the quantity delivered into the mixer. Material left on surfaces, retained in a line or falling after the feeder stops can create a difference. Specify the expected batch range and the test method before treating two accuracy figures as comparable.
Different ingredients create different control problems
Cement, lime and other dry binders
Cement and lime affect the chemistry and development of the AAC mix. Inaccurate dosing can alter slurry behavior and contribute to variation in the finished product. Lime is especially sensitive not only to quantity but also to its characteristics, including reactivity. A correctly weighed lime dose will not necessarily behave like the previous delivery if the material itself has changed.
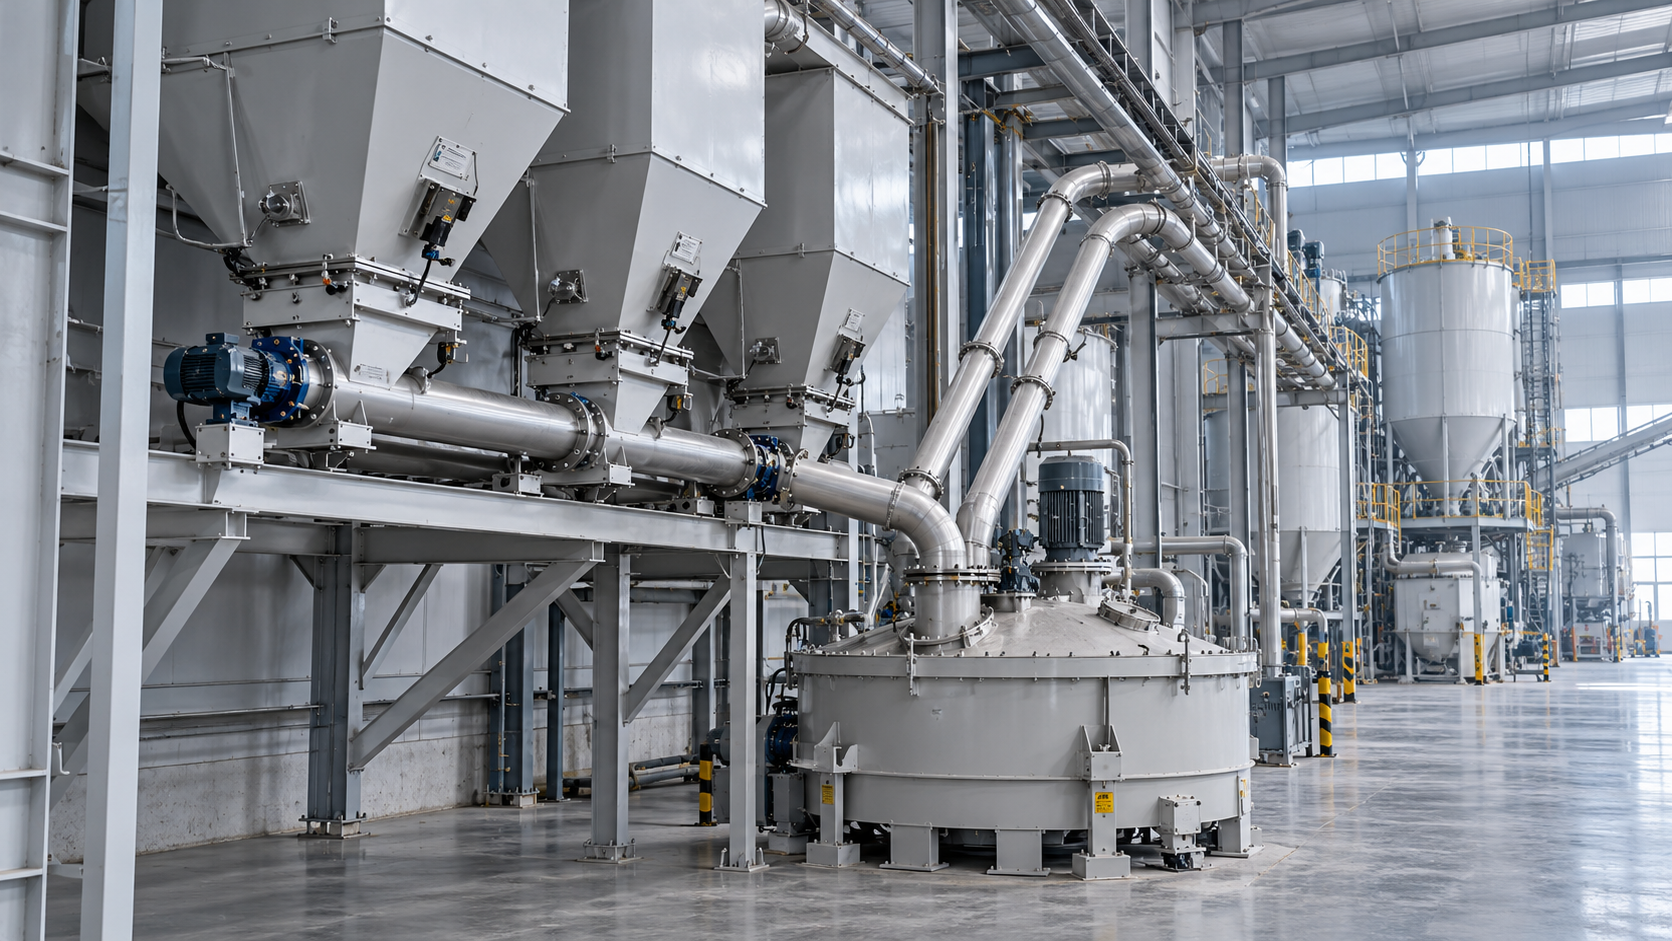
Dry powders also present mechanical challenges. Bridging, inconsistent screw-feeder flow, dust buildup and material remaining in the discharge path can all affect the delivered quantity. Coarse-and-fine feeding, where the system reduces the feed rate as it approaches the target, can help limit overshoot. Its effectiveness still depends on the material and the response time of the equipment.
Sand slurry, fly ash and recycled material
AAC plants may use ground sand slurry, fly ash or other suitable siliceous materials, depending on the formulation and local supply. For a slurry, total weight alone is not enough: the proportion of solids and water must also be understood. If slurry solids change while the same wet weight is dosed, both the solids delivered to the mix and the water balance change.
For example, a heavier slurry dose does not automatically mean more effective siliceous material if its solids concentration is lower. Operators need a reliable way to check slurry concentration and adjust the recipe or water addition accordingly. Where recycled AAC slurry is used, its solids content and consistency also need attention; otherwise, a useful recovery stream can become a source of batch variation.
Water
Water should be managed as a total mix balance, not merely as the reading on a water meter. Water can enter with slurry, recycled material and other wet ingredients. The amount intentionally added at the mixer may therefore need adjustment as incoming material conditions change.
Too much or too little water can change flow and setting behavior, affecting how the mix rises and how the green cake handles during cutting. A precise meter is useful, but it cannot compensate for an inaccurate estimate of water already present in the other ingredients. Measurement method, temperature, meter installation and maintenance should be considered together.
Aluminum powder or suspension
Aluminum is added in a relatively small quantity to generate gas and form the cellular structure of AAC. Because the addition is small, a modest absolute dosing error can become a substantial relative error. Variation may show up in cake rise, pore structure or density, although those outcomes also depend on temperature, mixing, material chemistry and timing.
If aluminum is prepared as a suspension, control includes more than weighing the original material. Concentration, mixing before dosing and the quantity actually transferred to the mixer all matter. The method must follow the material supplier’s handling and safety instructions; powder and suspension systems have different operating considerations.
Set tolerances from the process backward
A good specification begins with the product and recipe rather than an impressive number in an equipment brochure. Start with the required product grade and the applicable test requirements in the destination market. Then establish a baseline recipe using representative raw materials, and determine which variations the process can tolerate without producing unacceptable results.
For an existing line, review actual batch records alongside cake behavior, cutting performance and finished-product test results. If density varies, look for patterns in slurry solids, aluminum delivery, water addition and temperature before assuming a single scale is responsible. A dosing system can be accurate while another part of the process is drifting.
For a new line, the equipment supplier and process team should agree on provisional ingredient tolerances, then verify them during commissioning with the materials and batch sizes intended for production. Those limits may need refinement after trial batches. Tightening every tolerance indiscriminately can add cost and complexity without addressing the actual source of variation.
A useful specification should state:
- The target and operating range for each ingredient, including the smallest expected dose.
- Whether tolerance is expressed against target quantity, full scale or another reference.
- Whether acceptance is based on indicated weight, delivered quantity or both.
- The number and conditions of test batches, including normal production feed rates.
- How slurry solids, water already present in materials and retained material will be accounted for.
- What happens when a batch falls outside the agreed limit: alarm, hold, correction or rejection.
Where dosing systems lose accuracy in practice
A load cell may be functioning correctly while the weighing assembly is not. A hopper touching a fixed frame, a tight pipe connection or accumulated material can interfere with the load path. Vibration from nearby machinery may also disturb readings. Mechanical installation and routine inspection are therefore part of measurement control, not just maintenance details.
Feeder shutdown is another common source of error. When a screw, valve or pump receives a stop signal, material already in motion may continue to enter the hopper or mixer. A control system can compensate for this in-flight material, but the correction should be checked when material flow properties, feed rates or equipment condition change.
Water and slurry lines introduce their own issues: air, deposits, leaks and inconsistent line filling can affect measurement or delivery. The location of a meter matters too. A meter may record a transfer accurately while material remains in a pipe instead of reaching the mixer during the intended batch.
Automation helps only when operators can see what actually happened. A batch record should distinguish target values from actual values and flag manual corrections. Repeated small adjustments by operators may reveal a feeder problem or raw-material change that would otherwise be hidden by an apparently successful final weight.
Calibration is necessary, but delivered-dose checks close the gap
Calibration establishes whether an instrument measures correctly under defined conditions. It does not, on its own, prove that the entire dosing path delivers the right amount to the mix. Plants should combine calibration with practical checks appropriate to each ingredient and installation.
For a weighing hopper, this includes checking zero, using suitable reference weights or an agreed verification method, and inspecting the supports and connections. For a liquid meter, verification should consider the expected flow range and fluid properties. For small aluminum doses, the check should reflect normal preparation and transfer conditions, rather than weighing a dry sample in isolation if the plant actually doses a suspension.
Frequency should be based on equipment instructions, operating conditions and the consequences of error. Investigate after maintenance, a collision, a significant material change or unexplained product variation rather than waiting for the next scheduled check. Keep records of adjustments so the team can distinguish a one-off fault from gradual drift.
Evaluating a batching solution for an AAC line
The best dosing arrangement is the one that matches the production process. Capacity matters, but so do the smallest recipe quantities, the number of mixes, available space, cleaning access and the variability of local raw materials. An oversized common scale may be convenient for bulk ingredients while offering poor control over small additions; separate measurement paths may be more appropriate.
The batching system must also coordinate with the mixer and casting cycle. A feeder that reaches its target accurately but delays the batch can create pressure to bypass controls. Conversely, faster dosing is of limited value if it repeatedly overshoots or leaves operators correcting batches by hand. Ask suppliers how the system handles slow feed, overshoot, interrupted batches and recipe changes.
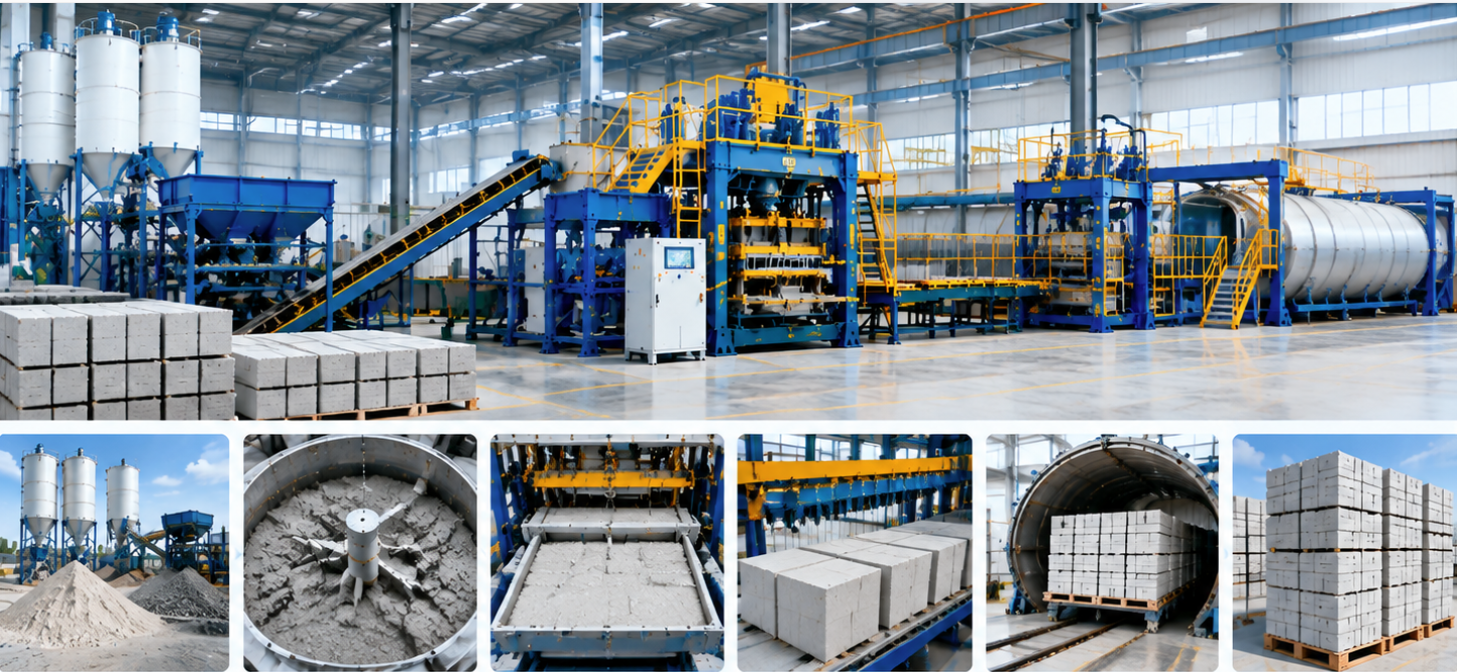
Shandong Hongfa Scientific Industrial & Trading Co., Ltd. manufactures AAC production lines as well as concrete batching plants. In discussions about a line, that equipment scope provides a basis for considering dosing alongside mixing, casting and downstream operations rather than treating the scale as an isolated purchase. The relevant design and performance commitments should still be confirmed against the specific project and its raw materials.
Before approving a system, prepare a material list with expected moisture or slurry-solids variation, intended batch sizes, product grades and available production space. Use it to agree on measurable acceptance tests and the responsibilities for calibration, commissioning and operator training. That gives the question of dosing accuracy a practical answer: not the smallest figure on a datasheet, but a verified level of control that the plant can maintain in everyday production.
Recommend
 Nov 03, 2026
Do You Need a Ball Mill for Sand-Based AAC Production?
Do I need a ball mill for sand-based AAC production? Discover when grinding is essential, when you can skip it, and how to make a cost-effective choice.
- Nov 03, 2026
How Accurate Should AAC Ingredient Dosing Be?
How accurate should AAC ingredient dosing be? Discover ingredient-specific tolerances, practical checks and batching tips to improve consistency and reduce waste.
 Oct 26, 2026
AAC Plant Technical Training: Operator Skills to Verify Before Startup
AAC plant technical training: Discover essential operator checks for dosing, cutting, and autoclave safety. Reduce startup waste and verify team readiness with practical competency assessments.