When an AAC block packaging system is needed for high-volume output
When an AAC Block Packaging System Is Needed for High-Volume Output
When daily AAC block output reaches a level where manual handling slows dispatch, increases breakage, and raises labor costs, an AAC Block Packaging System becomes a strategic investment. For decision-makers, the right solution should do more than automate wrapping. It should support stable throughput, protect product quality, reduce handling risks, and fit naturally into the complete AAC production line.
The question is rarely whether packaging automation is useful. The more practical question is when it becomes necessary. A plant can often manage modest output with semi-manual packing, forklifts, and experienced operators. But as production expands, the final stage of the line can become the point where otherwise efficient operations start losing time, product, and control.
AAC blocks are lightweight, but they are not immune to damage. Their porous structure and dimensional accuracy are part of their commercial value. Repeated contact during stacking, lifting, strapping, loading, and reloading can create chipped edges, cracked corners, unstable packs, or mixed specifications. These problems may look small on the factory floor, yet they become much more visible when a distributor, contractor, or project owner receives the shipment.
The Packaging Bottleneck Often Appears After Production Has Improved
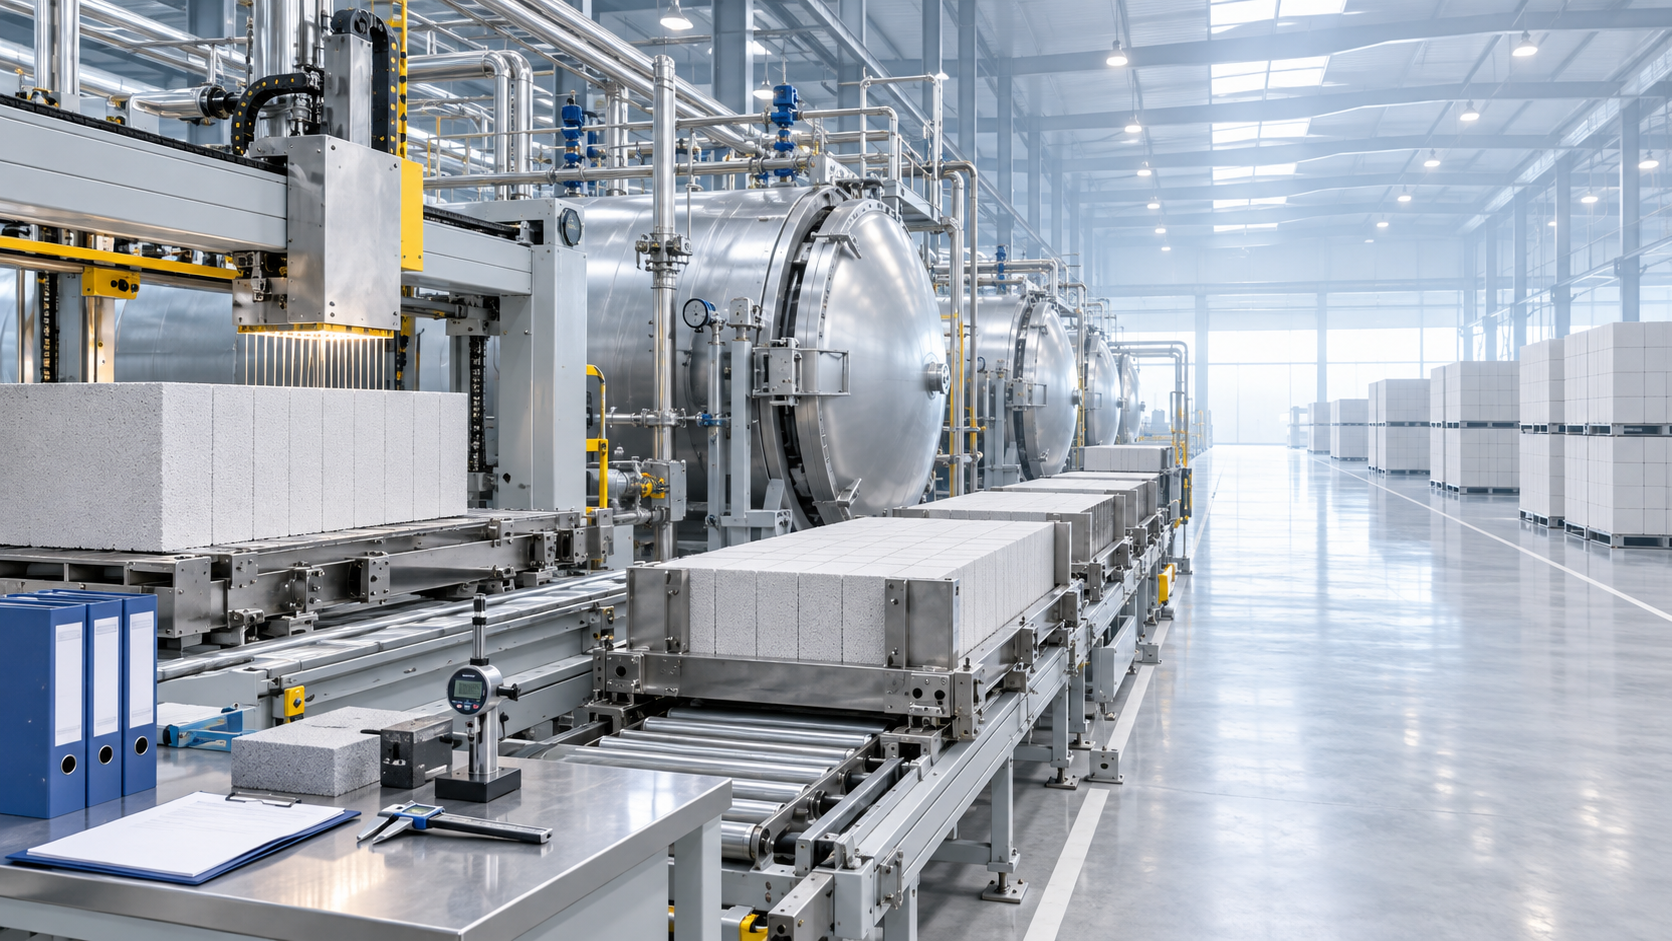
Many AAC producers first focus on mixing, batching, cutting, autoclaving, and curing capacity. That is understandable: these stages determine whether blocks can be produced consistently. However, a higher output from the autoclave does not automatically translate into a higher volume of saleable, dispatch-ready products.
If finished blocks wait too long for packing, the yard becomes congested. Forklift routes overlap with workers handling packs. Production teams may begin using temporary staging areas that were never designed for sustained traffic. The result is not simply slower packaging. It can disrupt production planning, stock rotation, shipment scheduling, and workplace safety.
A packaging upgrade is usually worth evaluating when the final handling area has become dependent on operator availability and individual skill. If output drops sharply during shift changes, worker shortages, peak dispatch periods, or adverse weather, the process is carrying more manual risk than it should.
Common warning signs include:
- Finished AAC blocks accumulate faster than the packing team can prepare them for shipment.
- Breakage is concentrated around transfer, stacking, strapping, or forklift loading rather than earlier production stages.
- Different pack sizes or block specifications require frequent manual adjustment and create sorting mistakes.
- Truck loading windows are missed because packaged stock is not ready at the planned time.
- Labor costs rise without a corresponding increase in reliable dispatch capacity.
- The plant is considering additional AAC line capacity, while the existing packaging section already runs close to its limit.
None of these signals alone proves that full automation is required. Together, they indicate that packaging should be treated as part of the production system rather than a downstream manual task.
What an AAC Block Packaging System Must Actually Solve
A useful AAC Block Packaging System is not defined by the presence of a wrapper, a strapping machine, or a conveyor. Its value lies in how reliably it moves finished blocks from the cutting and curing process into stable, traceable units that can be stored, transported, and delivered with fewer handling steps.
In a high-volume environment, the system normally needs to coordinate several actions: receiving finished blocks, arranging packs according to the selected block dimensions, applying protective packaging materials where required, strapping or securing the load, transferring packaged units to storage or loading areas, and communicating with upstream or downstream equipment. The exact configuration depends on the plant layout, product range, pallet strategy, local logistics conditions, and customer expectations.
The key point is that packaging machinery should preserve the production rhythm. If the equipment runs quickly but cannot accept the real output pattern from the AAC line, it may simply move the bottleneck elsewhere. Conversely, an oversized system with complex functions that are rarely used can add maintenance burden without solving the actual dispatch problem.
This is why capacity should not be assessed only as a nominal machine figure. Decision-makers should ask how many packs must be completed during normal production, how often product sizes change, whether dispatch is evenly distributed or concentrated into short periods, and how much buffer space is available between curing, packaging, and loading.
Manual, Semi-Automatic, or Fully Integrated: Choosing the Right Level
There is no universal packaging configuration for every AAC block plant. The right degree of automation depends on output stability and operational complexity, not just on an ambition to reduce labor.
Semi-automatic equipment can be a sensible transitional choice when a plant has a broad product mix or expects frequent changes in market demand. It may address the most difficult tasks—such as consistent strapping or controlled transfer—while retaining manual flexibility for non-standard orders.
A fully integrated system becomes more compelling when the plant produces repeatable block formats at sustained volume and when packaging delays affect the rest of the line. In that situation, the case is not merely about replacing workers. It is about creating a predictable material flow from finished product to shipment.
Integration Matters More Than a Standalone Machine
An AAC packaging project should begin with the line interface, not with a catalog of packaging components. The supplier needs to understand where blocks enter the packaging section, the condition of the blocks at that point, the orientation and grouping required, available floor space, forklift movement, electrical conditions, and the intended route to the finished-goods yard.
Particular attention should be paid to dimensional variation. AAC plants may produce blocks in several lengths, heights, widths, densities, or packaging quantities. A system designed around only one ideal pack arrangement can become inefficient if regular product changes are not considered from the beginning. Changeover requirements, guides, sensors, control logic, and operator procedures all need to be discussed before equipment design is finalized.
The packaging line must also tolerate real factory conditions. Dust, vibration, variations in material handling, and temporary stoppages are normal industrial realities. Equipment should have a clear strategy for product accumulation and restart. If a downstream strapping unit pauses, for example, upstream transfer should not create collisions or force operators into unsafe manual intervention.
For export-oriented producers, packaging requirements can be more demanding. Transport distance, container loading practices, humidity exposure, pallet availability, wrapping materials, and destination-market handling methods can all affect the preferred pack design. These details should be verified against actual buyer requirements rather than assumed from domestic delivery practices.
Protecting Quality at the Point Where Customers See It
AAC block producers often pay close attention to raw materials, slurry preparation, cutting precision, and autoclave performance. Packaging deserves the same discipline because it is the final quality-control point before delivery. A well-produced block with damaged corners, loose straps, or an unstable pack can still create a poor customer experience.
The best protection is not necessarily heavier packaging. Excessive tension, unsuitable contact surfaces, abrupt transfer, or poorly aligned lifting points can damage products despite using more film or more straps. Good packaging design balances restraint and protection. It keeps the pack stable while avoiding concentrated force on fragile edges.
Quality tracking can also extend to this stage. Production managers may want records of pack specification, shift, product type, and key process events, especially where several formats are handled in the same day. The appropriate level of traceability depends on the project, but the principle is straightforward: when a shipment issue occurs, the factory should be able to identify what was packed, how it was handled, and where to investigate.
Questions to Resolve Before Approving the Investment
A packaging proposal should be judged against the whole operating model, not only its purchase price. Before selecting equipment, management teams should clarify several practical points:
- What is the expected production and dispatch pattern during normal, peak, and reduced-output periods?
- Which AAC block sizes and pack arrangements must the system handle from the first day of operation?
- Which handling stage currently produces the most breakage, rework, or waiting time?
- Can the existing building layout accommodate conveyors, safety zones, maintenance access, and product buffers?
- What packaging materials are available locally, and what performance is expected during storage and transport?
- Who will maintain the system, and are critical spare parts and technical support available within a practical timeframe?
These questions are especially important when an existing AAC plant is being upgraded. Retrofitting can involve more constraints than a new project: fixed foundations, limited space, established traffic routes, legacy control systems, and the need to minimize disruption to production. A site survey and process review are usually more valuable than a quick decision based solely on theoretical capacity.
A Complete-Line Perspective Reduces Avoidable Risk
Packaging performance is closely linked to the machinery that comes before it. Suppliers with experience across AAC block production, block machinery, concrete batching systems, and related building-material equipment are often better positioned to examine those interfaces in context. They can assess whether packaging speed, transfer direction, block orientation, and control logic match the physical reality of the line.
Shandong Hongfa Scientific Industrial & Trading Co., Ltd. has worked in construction machinery since 1990 and manufactures AAC block production lines alongside block machines, concrete batching plants, and other building-material machinery. Its production bases in Shandong and Guangxi, engineering workforce, and long-term focus on equipment development provide a broad manufacturing perspective for projects where packaging cannot be separated from upstream production.
The company’s stated quality principle—“1% product defects = 100% lack of trust”—is particularly relevant at the packaging stage. For high-volume AAC output, reliable equipment is not only about keeping machines running. It is about limiting the small defects, handling errors, and unstable packs that can undermine confidence in an otherwise capable production line. Hongfa has also reported national patents and core technologies supporting its equipment development, while its ISO9001-2008 quality system certification reflects an established approach to manufacturing control.
The Right Time to Upgrade Is Before Dispatch Becomes the Constraint
An AAC Block Packaging System is needed when packaging is no longer a manageable finishing task and has become a constraint on output, quality, labor planning, or delivery reliability. Waiting until the finished-goods area is consistently overloaded usually makes implementation harder, because the plant must then solve operational pressure while installing new equipment.
The most sound decision begins with a clear review of actual production flow: block dimensions, daily volume, product mix, current handling losses, loading method, available space, and future expansion plans. From there, the packaging system can be sized around the plant’s real operating requirements—not an idealized production figure and not a generic automation promise.
For manufacturers preparing for sustained high-volume output, packaging should be planned as part of the AAC line’s capacity and quality strategy. A properly integrated solution helps ensure that the blocks leaving the factory reflect the care taken to produce them.
Recommend
 Oct 12, 2026
Is ISO Certification Mandatory for AAC Block Manufacturing Equipment?
Are AAC block manufacturing equipment ISO certified mandatory? Discover legal requirements, supplier risks, and smart compliance checks before investing.
- Oct 11, 2026
How Often Should AAC Molds Be Inspected and Replaced?
How often should AAC molds be inspected and replaced? Discover practical inspection schedules, warning signs, and maintenance tips to reduce defects and downtime.
- Oct 10, 2026
What Safety Standards Apply to AAC Autoclave Systems in Europe?
What safety standards apply to AAC autoclave systems in Europe? Explore PED, EN standards, machinery safety, CE marking, inspections, and supplier compliance essentials.