How Can Buyers Assess Hongfa AAC Plant Commissioning Quality?
Hongfa AAC plant commissioning service quality is best assessed through witnessed production trials, traceable test results, and a handover package that proves the plant is ready for routine operation. Machinery movement alone establishes very little. Acceptance should connect safe equipment operation with repeatable batching, stable cake development, accurate cutting, controlled autoclaving, and finished blocks that meet the agreed specification.
The strongest evidence follows an identifiable batch from raw material preparation to finished-product testing. That connection makes it possible to distinguish an equipment fault from a recipe problem, a utility limitation, or an adjustment that worked only under unusually favorable conditions.
What evidence should be agreed before commissioning begins?
A written acceptance protocol should define the products, raw materials, operating conditions, and measurements used to judge performance. Without that agreement, a successful trial could mean anything from completing an automatic sequence to producing saleable blocks at the contracted output.
The protocol needs clear boundaries: which equipment is included, where utilities enter the supplied system, which laboratory tests establish product acceptance, and how interruptions affect the performance trial. It should also identify who witnesses results and who has authority to approve deviations.
Useful acceptance criteria connect a measured result with its test conditions:
- Product conformity: specified dimensions, dry density, compressive strength, and other properties required by the purchase agreement, assessed using the agreed sampling and test methods.
- Production performance: saleable output over a defined period, with rejects, recycled material, stoppages, and work in progress accounted for.
- Operating readiness: demonstrated safety functions, completed maintenance instructions, and successful operation by the designated site personnel.
Any prerequisite outside the commissioning scope, such as steam availability or laboratory readiness, should have a recorded status before performance testing starts.
How much does a successful dry run actually prove?
A dry run establishes that drives, sensors, actuators, and control sequences behave as intended without process material. It provides useful evidence of installation and integration quality, but it cannot establish cake stability, cutting performance under load, or finished-block strength.
Observe equipment interfaces closely. Mold positioning must match filling and transfer requirements; cutting equipment must receive cakes in the correct orientation; transfer devices must complete their movements without collision or uncontrolled impact. Repeated manual intervention at these interfaces suggests that automatic production is not yet stable.
Alarm testing should demonstrate both detection and response. A low-level signal, an unavailable downstream station, or a failed position confirmation should produce the documented system behavior. Record the initiating condition, displayed alarm, resulting equipment state, and recovery procedure.
Safety functions require controlled verification by qualified personnel using approved procedures. Emergency stops, guards, pressure-system permissives, and restart behavior need specific records. A signed statement saying “electrical system tested” provides too little detail to establish what was verified.
Which process measurements reveal whether the startup is stable?
AAC performance depends on relationships between materials and process settings. A mixing time or slurry temperature has limited meaning without the associated recipe, material condition, and cake-development record.
For sand-based production, slurry preparation should establish suitable fineness and consistency. For fly ash-based production, variation in incoming material also deserves attention. Lime reactivity, cement condition, gypsum characteristics, aluminum dosing, and water temperature influence how the mixture rises and gains enough green strength for cutting.
Records should distinguish recipe setpoints from actual measured quantities. A correctly displayed dosing target does not prove that the weighing system delivered it. Scale verification, repeatability, zero stability, and material remaining in discharge paths all affect the real batch.
A commissioning report becomes more useful when it explains why settings changed and shows whether the adjustment remained effective in subsequent batches.
How should trial blocks be sampled and evaluated?
Trial production should include representative samples from identifiable batches and positions within cakes or loads. Selecting only visually attractive blocks conceals variation and weakens the acceptance result. Sampling locations and selection methods should be agreed before production results are known.
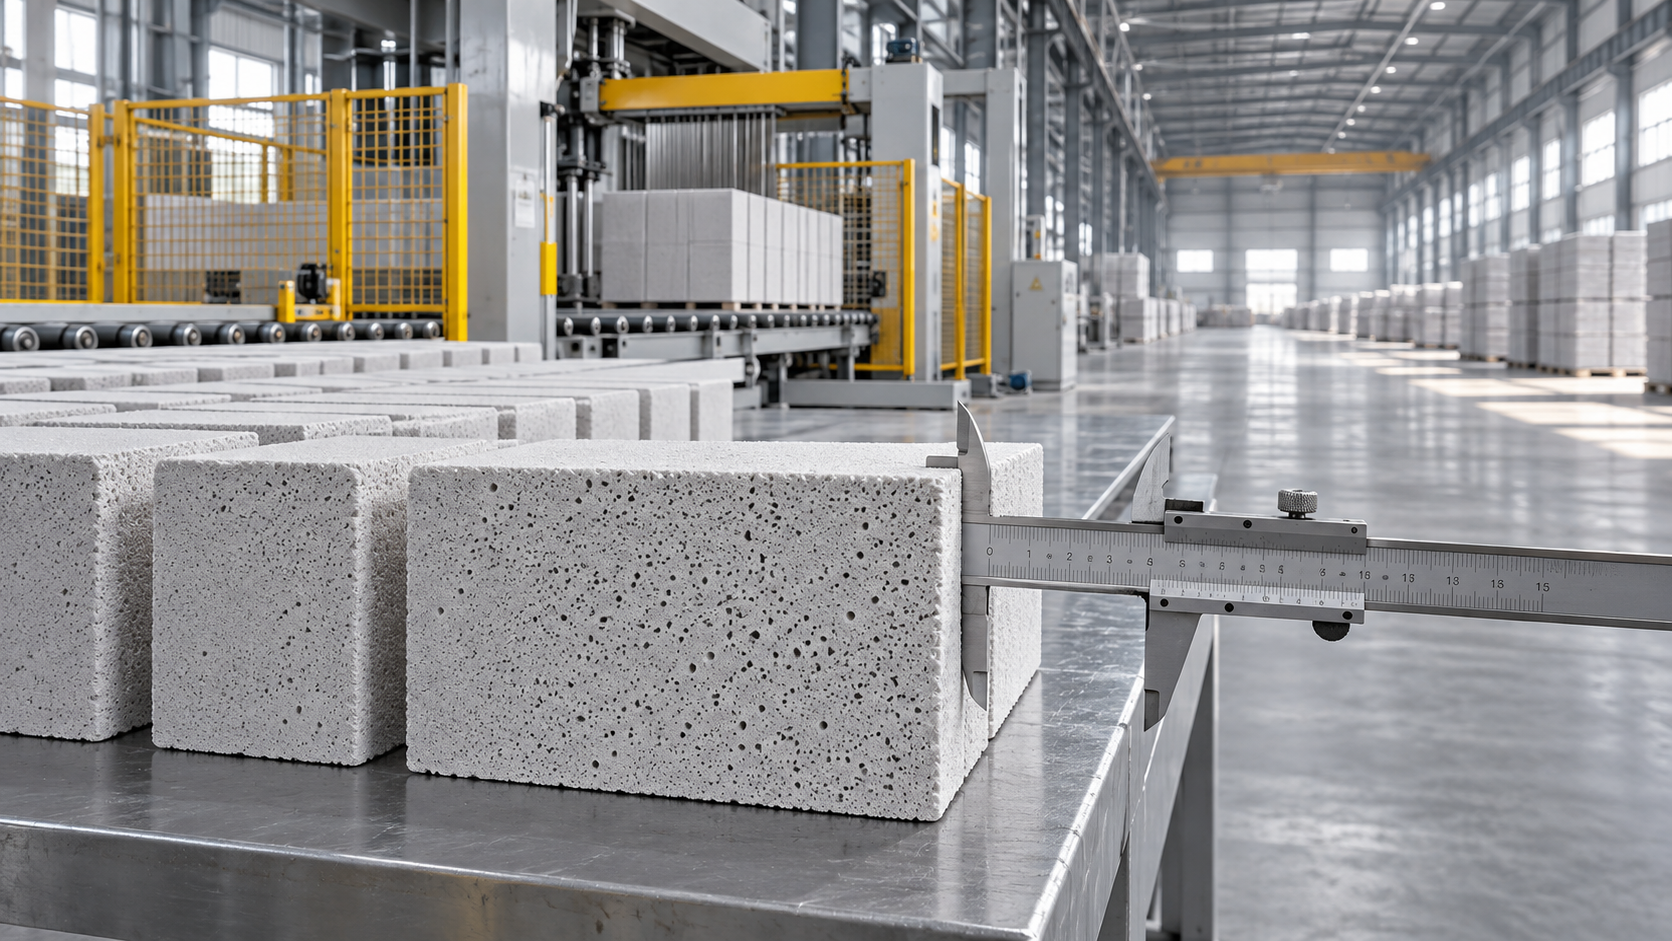
Dimensional measurements should address the specified tolerances and reveal patterns. Repeated errors in one direction suggest a different problem from random damage concentrated near cake edges. Cutting accuracy, wire movement, cake condition, and handling damage should be investigated separately.
Density and compressive strength require particular care. Freshly autoclaved blocks contain moisture, so an immediate mass measurement cannot be treated as dry density. Strength results also require consistent specimen preparation and conditioning under the agreed test method. Results from different conditions are not directly comparable.
Visual inspection remains useful for identifying cracks, broken corners, sticking between blocks, and surface defects. However, appearance cannot establish internal performance. Each laboratory result should retain its batch reference, sampling location, test date, and conditioning details so that an apparent failure can be traced back to production conditions.
What demonstrates acceptable autoclave commissioning?
An autoclave trial should demonstrate the approved operating sequence under representative loading conditions. Reaching a displayed pressure does not, by itself, establish that the load received the intended curing treatment.
Review the recorded pressure and temperature histories alongside air removal, steam admission, holding, depressurization, and condensate handling. Sensor location matters when interpreting these records. A vessel measurement describes conditions at that measurement point; product tests provide additional evidence of how the curing cycle affected the blocks.
The load arrangement should match the configuration intended for production. A lightly loaded trial provides limited evidence for a fully loaded vessel because steam distribution, heating demand, and condensate behavior change with the load.
Door locking, pressure indication, protective devices, and opening permissives require documented verification under the applicable procedures. These tests belong with qualified personnel and approved methods. Where steam recovery is included, commissioning should also establish that transfer between vessels follows the intended sequence without disrupting the receiving cycle.
Can one good batch justify performance acceptance?
One conforming batch shows that acceptable production is possible under the conditions recorded. Repeatability requires evidence across consecutive batches and complete production cycles, with the trial duration defined in the acceptance agreement.
The trial should expose the plant’s main constraints. A short run can finish before mold circulation becomes limiting or before autoclave availability creates a queue. Output measured only at the cutting machine leaves these restrictions unresolved.
Saleable output should be measured at the agreed production boundary. The record needs a consistent treatment of rejects, broken blocks, recycled material, and unfinished inventory. Otherwise, material accumulated between stages can make temporary output appear sustainable.
Interruptions also need classification. Equipment faults, material shortages, utility interruptions, planned sampling, and operating errors have different implications. A shared event log should record their duration, cause, and treatment in the acceptance calculation.
If significant changes are made during the run, document which results belong to each operating condition. Combining output from several recipes or control settings into one average can hide whether the final configuration achieved the agreed performance.
How can training quality be demonstrated?
Attendance sheets establish that training occurred. Practical demonstrations establish whether the knowledge transferred.
During supervised production, the designated operating personnel should carry out startup, recipe selection, routine sampling, controlled shutdown, and recovery from approved simulated faults. Their responses should follow written instructions and preserve the required safety conditions.
Maintenance training needs similar practical content: identifying lubrication points, inspecting cutting wires, recognizing wear, applying isolation procedures, and finding the correct replacement part in the documentation. Tasks involving pressure equipment or electrical work must respect the site’s competence and authorization requirements.
A useful training record identifies the task performed, the person demonstrating it, any assistance required, and unresolved gaps. Repeated reliance on the commissioning engineer for ordinary sequence recovery indicates that handover readiness remains incomplete, even when production results are acceptable.
What should the final handover package contain?
The handover package should describe the plant as commissioned. Early drawings, generic manuals, and untracked parameter sheets leave uncertainty about the actual installation.
Essential records include the agreed acceptance protocol, signed trial results, instrument verification records, batch and laboratory data, safety-function test records, and an outstanding-item register. Equipment identification must remain consistent across drawings, control screens, maintenance instructions, and spare-parts lists.
Control-system backups should correspond to the accepted configuration, with software versions and access arrangements documented. Process recipes need revision identification and clear limits on authorized adjustment. Changes made during commissioning should appear in the final settings and drawings.
The outstanding-item register should identify each defect, its operational effect, corrective action, responsible party, and required evidence for closure. It should also distinguish a documentation correction from a fault affecting safe operation or product conformity. Any deferred performance test needs its own agreed conditions and completion record.
When is conditional acceptance reasonable?
Conditional acceptance is reasonable when unresolved items have a defined effect and the agreement clearly states how they will be closed. It becomes difficult to defend when essential safety evidence, representative product results, or required performance trials are missing.
For example, an incomplete drawing revision and an unverified autoclave protective function carry very different consequences. Treating both as ordinary punch-list items obscures the basis for operating the plant.
Closure should require evidence appropriate to the defect. A corrected label can be confirmed by inspection; a dosing fault requires verified measurement and relevant production results. Where an equipment change affects downstream behavior, repeat the affected integrated trial rather than closing the item solely because the replacement component runs.
The acceptance signature should refer to a specific configuration, a defined set of test results, and any explicitly recorded reservations. That creates a usable technical record for resolving later production problems and determining whether the commissioned plant met the agreed conditions.
Recommend
 Oct 30, 2026
Which Hongfa Hydraulic Brick Machine Specifications Should Buyers Check?
Compare Hongfa hydraulic brick making machine specifications, from forming pressure and output to molds and power demand. Discover what to verify before investing in your production line.
- Oct 30, 2026
How Can Buyers Assess Hongfa AAC Plant Commissioning Quality?
Assess Hongfa AAC plant commissioning service quality through production trials, block testing, safety checks, and handover records. Learn what to verify before accepting your plant.
- Oct 29, 2026
What Export Experience Does Shandong Hongfa Building Machinery Have?
Assess Shandong Hongfa building machinery export experience through project records, delivery planning, and after-sales support. Discover what to verify before your next equipment purchase.