How Do You Calculate a Concrete Brick Machine’s Production Capacity?
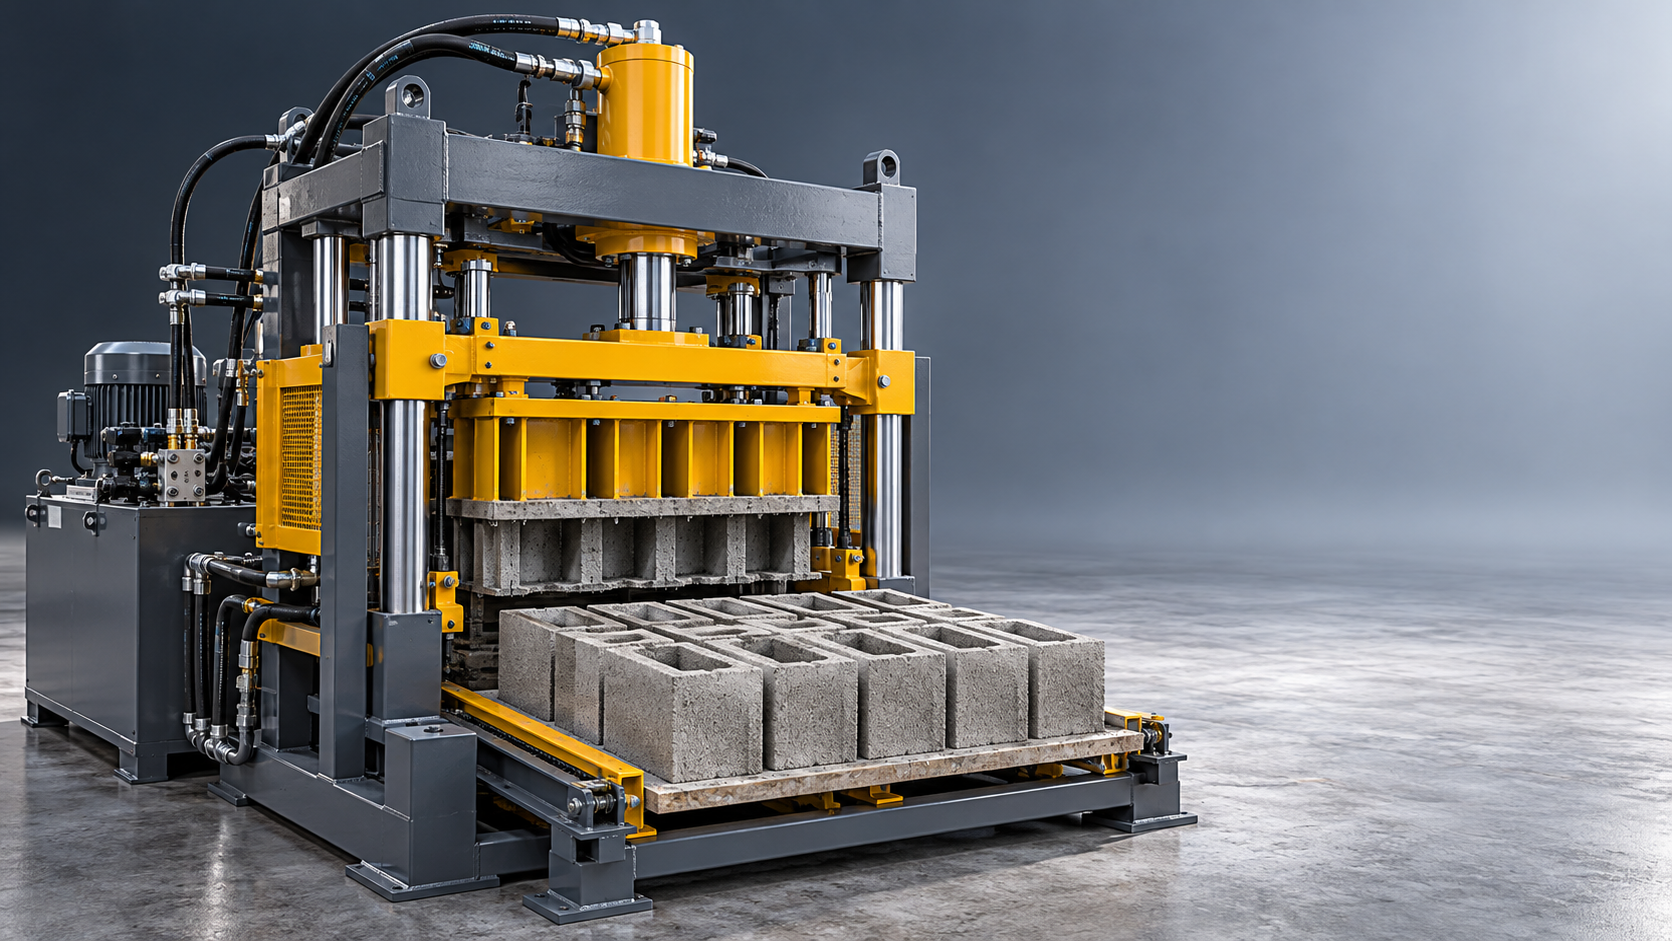
A concrete brick machine’s production capacity is calculated from the number of units produced per molding cycle and the number of cycles completed per hour. To estimate usable daily output, that theoretical figure must then be adjusted for scheduled operating time, downtime, reduced running speed, and rejected products.
The essential distinction is between maximum molding output and sustainable, saleable production. A machine may achieve its advertised cycle time during uninterrupted operation, yet the complete line can deliver less because of material shortages, pallet circulation, handling delays, or curing constraints. A useful capacity calculation makes those limits visible rather than hiding them inside a single “bricks per day” figure.
The basic production capacity formula
For one product made with one mold configuration:
Theoretical hourly output = Units per cycle × 3,600 ÷ Cycle time in seconds
If a mold produces 12 concrete bricks per cycle and the complete cycle takes 20 seconds:
- Cycles per hour = 3,600 ÷ 20 = 180
- Theoretical hourly output = 12 × 180 = 2,160 bricks
- Theoretical output over eight hours = 2,160 × 8 = 17,280 bricks
These figures assume continuous operation at the stated cycle time, with every mold cavity producing an acceptable unit. They do not yet account for stoppages, slower cycles, changeovers, or quality losses.
For planning purposes, the expanded calculation is:
Expected good output = Units per cycle × (3,600 ÷ Reference cycle time) × Planned production hours × Availability × Performance × Quality yield
All three adjustment factors are expressed as decimals. Their definitions matter: applying overlapping allowances can understate capacity just as easily as ignoring losses can overstate it.
Confirm what “units per cycle” actually means
The correct starting value is the number of finished units molded during one complete production cycle—not the number of cavities associated with a different product or an alternative mold.
The same machine can produce different quantities of small solid bricks, hollow blocks, and paving units per cycle. Output depends on usable molding area, product dimensions, mold layout, and equipment limits. A machine’s model designation alone is not sufficient evidence of capacity.
Record the exact product dimensions, mold configuration, and number of units per production pallet. Also confirm whether the quoted quantity refers to individual units, pallets, or square meters of paving. These measures cannot be compared directly.
When converting paving output into area, use the specified coverage per unit, including the agreed joint convention where relevant. When comparing hollow blocks by material consumption, do not use external dimensions as though each block were solid concrete. Its net concrete volume is different from its nominal envelope volume.
Use a complete cycle time, not an isolated machine movement
A short vibration time is not the same as a short production cycle. The relevant interval is the time between equivalent points in successive cycles—for example, from the start of one mold-filling operation to the start of the next.
Depending on machine design, that interval includes material feeding, vibration and pressing, demolding, pallet exchange, and any movements that must finish before another cycle begins. Some operations overlap, so adding every individual movement time can also produce an incorrect result.
Cycle time must correspond to the intended product and mix. Changes in unit height, mold geometry, filling behavior, or compaction requirements can change the achievable rate. Reducing the cycle is not a valid capacity improvement if it produces underfilled corners, dimensional variation, or inadequate product performance.
There are two sound calculation methods:
- Reference-cycle method: Use a demonstrated reference cycle time, then apply a performance factor to account for slower operation and minor interruptions.
- Measured-running method: Use an average observed cycle time during operation, then adjust separately for downtime and quality losses.
Do not apply a second speed-loss allowance if the measured average cycle time already includes that loss. Similarly, if an elapsed-time production measurement includes stoppages, applying the same downtime allowance again would double-count them.
A worked calculation: from rated output to good units per shift
Consider an illustrative machine producing 12 bricks per cycle at a reference cycle time of 20 seconds. The shift lasts eight hours, but 30 minutes are reserved for a planned break and cleaning period when production stops. Planned production time is therefore 7.5 hours.
Assume the remaining production window has 88% availability, 92% performance, and a 97% quality yield. These are calculation assumptions, not industry benchmarks.
The eight-hour theoretical figure was 17,280 bricks. Under the stated assumptions, expected good output is approximately 12,722 bricks per shift. The difference comes from explicitly identified time and quality losses, not from an arbitrary reduction of the advertised rating.
For production commitments, use a suitably rounded planning figure rather than treating the calculated result as a guaranteed exact count.
Keep the adjustment factors separate
Availability is operating time divided by planned production time. It accounts for stops such as breakdowns, material interruptions, and adjustments, according to the plant’s recording rules. In this example, the 30-minute planned exclusion has already been removed before availability is calculated.
Performance compares actual running output with the output possible at the reference cycle time during that operating time. It captures slower cycles and short interruptions not recorded as downtime. Each loss should belong to only one category.
Quality yield is acceptable units divided by total units produced. Define the inspection boundary: units accepted immediately after molding are not necessarily equivalent to units accepted after curing and handling.
The product of availability, performance, and quality is commonly used as overall equipment effectiveness, or OEE. An OEE percentage is meaningful only when its production-time boundaries and reference cycle are known.
Check whether the rest of the line can sustain the calculated rate
The molding machine sets one capacity limit; the complete production system may impose a lower one. Compare each stage on a consistent basis, such as equivalent units per hour for the same product.
Concrete mixing and delivery
Material demand should be calculated from gross molded output, because rejected units also consume material. If the theoretical rate is 2,160 units per hour and each unit contains an illustrative 0.004 cubic meters of compacted concrete, corresponding net demand is:
2,160 × 0.004 = 8.64 cubic meters per hour
This is a product-volume calculation, not a direct loose-material batching specification. The batching calculation must account for the mix, yield, moisture, and process losses. Hollow products require their actual net material content.
Compare demand with the mixer’s usable discharge volume and complete batch time, including charging, mixing, discharge, and transfer. Nominal mixer vessel volume alone does not establish sustained supply capacity. A buffer hopper can absorb timing differences, but it cannot compensate indefinitely for an undersized mixing system.
Pallet supply and green-product handling
If each cycle requires one production pallet, the 20-second reference cycle requires 180 pallets per hour. Pallet feeding, conveyors, elevators, and transfer equipment must support that cadence without damaging fresh products.
The circulating pallet requirement depends on how long each pallet remains unavailable:
Required circulating pallets ≈ Pallets consumed per hour × Pallet return time in hours
Add an allowance for cleaning, inspection, damaged pallets, and operating buffers. Where production stops overnight, calculate the maximum number tied up across the actual schedule rather than multiplying a continuous hourly rate by the entire elapsed curing period.
Pallet return time is not automatically the same as full curing time. It depends on when the product can safely be removed under the actual handling and curing process.
Curing and finished-product handling
Curing is a capacity constraint because products occupy positions before they can be released. Under steady operation, the relationship is:
Required occupied curing positions ≈ Incoming pallets per hour × Residence time in hours
For intermittent shifts, map actual arrivals and releases to find peak occupancy. Include transfer space and positions unavailable during loading or unloading.
Curing residence time cannot simply be shortened to accommodate higher machine output. Release must remain consistent with the product’s handling-strength requirements and applicable quality specifications. Downstream cubing, strapping, and storage transfers must also clear production fast enough to prevent congestion.
Where a downstream stage cannot keep pace, a larger press or shorter molding cycle will not deliver the corresponding increase in saleable output. It may only fill the available buffer sooner.
Calculate mixed-product schedules by time, not average unit counts
A daily plan containing several products needs a separate calculation for each mold and cycle time. Adding their nameplate hourly capacities or averaging their units per cycle produces a misleading result.
Total good output = Sum of each product’s expected good output during its allocated production time
Subtract mold changes, setup adjustments, cleaning, and trial production from the available schedule, unless those losses are already included in the chosen availability factor. Each product should retain its own quality yield where performance differs.
A shift producing 10,000 small bricks cannot be compared directly with one producing 5,000 larger blocks. Unit counts are useful for order fulfillment, but material throughput and occupied production time explain equipment loading more accurately.
Turn the calculation into a verifiable capacity requirement
A credible concrete brick machine production capacity claim should identify the product drawing, mold cavities, complete cycle time, operating schedule, and whether output means molded units or accepted finished products. It should also state which supporting equipment is included.
A capacity demonstration should run long enough to reveal repeated mixing, pallet exchange, and handling interactions. Recording only the fastest few cycles establishes a possible machine speed, not sustainable line output.
Useful records include elapsed time, completed cycles, total molded units, stoppage duration and causes, rejected units, and downstream accumulation. Quality acceptance should cover the agreed product requirements; visual acceptance immediately after demolding does not establish final performance after curing.
When operating history is unavailable, calculate several scenarios using explicit assumptions rather than presenting one efficiency percentage as fact. A lower-output scenario can test whether the production plan remains workable during slower operation or additional downtime.
The final planning number should be the achievable output of the constrained line, adjusted for quality—not simply the fastest theoretical output of the molding machine. Keeping the mold, time basis, loss categories, and acceptance point consistent makes that number useful for equipment comparison, production scheduling, and delivery commitments.
Recommend
 Oct 31, 2026
Which Is More Durable: Color Tile or Concrete Roof Tile?
Which is more durable: color tile or concrete roof tile? Compare materials, weather resistance, and manufacturing quality to choose the right roofing with confidence.
- Oct 31, 2026
What Does Hongfa AAC Factory Planning Consulting Include?
Explore what Hongfa AAC factory planning consulting should cover, from raw materials and layouts to utilities and deliverables, to make informed investment decisions.
- Oct 30, 2026
Which Hongfa Hydraulic Brick Machine Specifications Should Buyers Check?
Compare Hongfa hydraulic brick making machine specifications, from forming pressure and output to molds and power demand. Discover what to verify before investing in your production line.