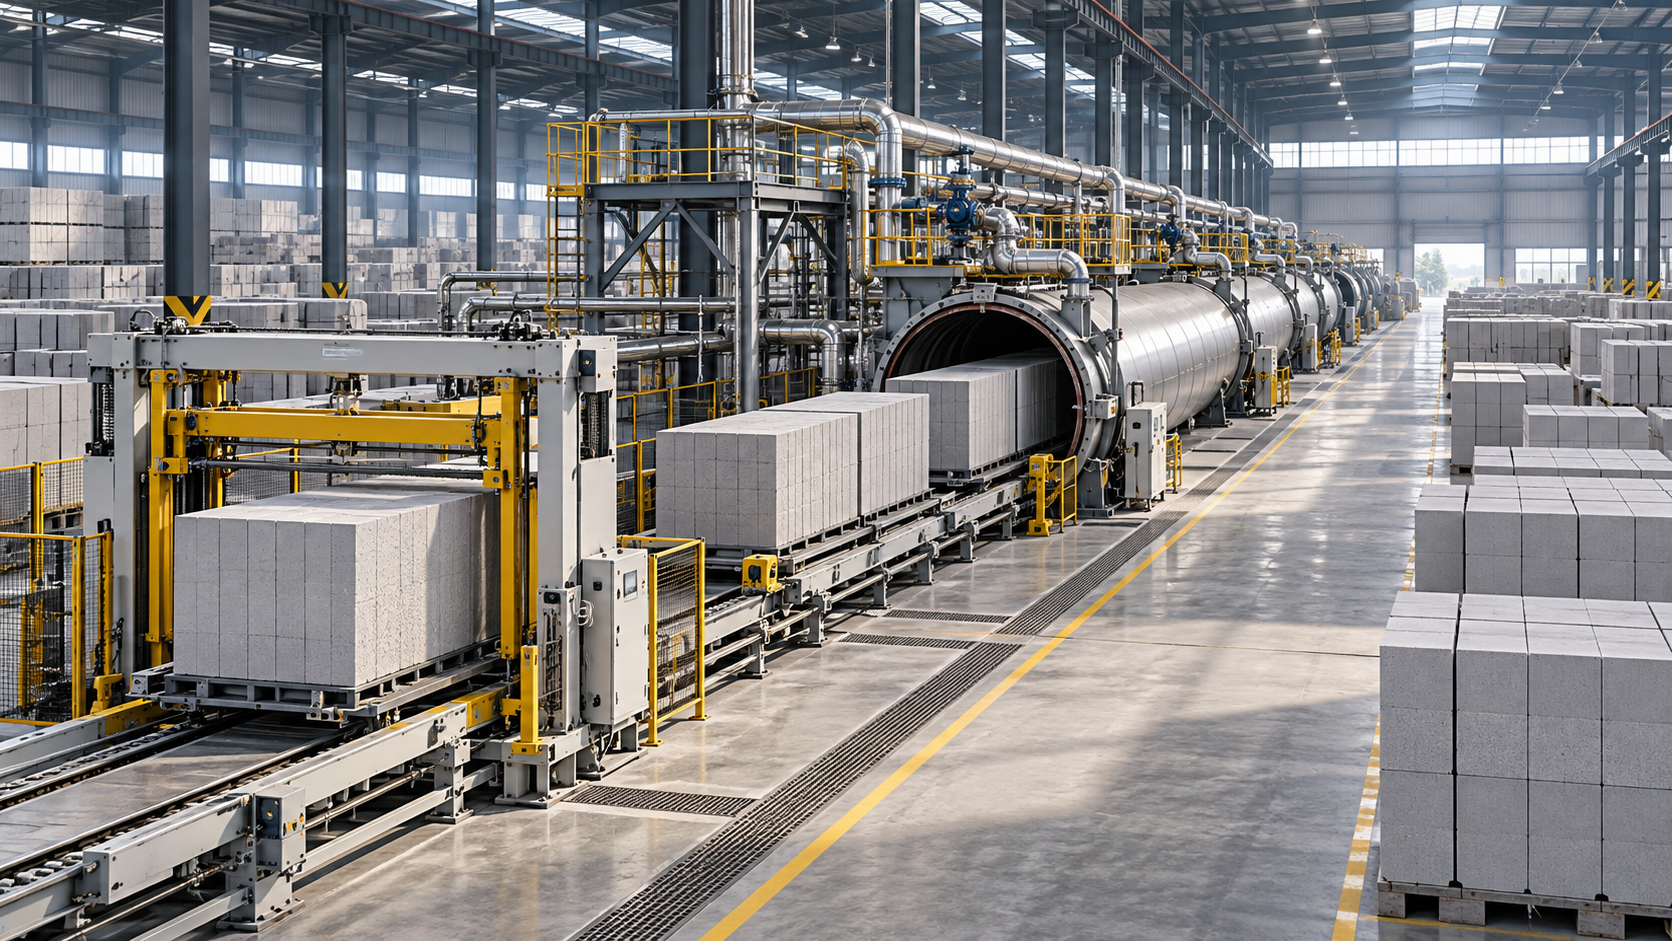
AAC Autoclave System Safety: Pressure Vessel Codes and Inspection Needs
An AAC autoclave system needs two separate compliance checks: whether the pressure vessel was designed and manufactured under a code accepted at its installation site, and whether the operating plant meets local inspection and safety requirements. A code stamp, conformity marking, or factory pressure-test report can support the first check. None, by itself, establishes that the installed system is safe to operate throughout its service life.
For quality control and safety teams, the practical task is to connect the vessel’s design limits with its actual operating conditions, protective devices, inspection history, and maintenance records. The highest-priority issues are the applicable jurisdiction, the condition of the pressure boundary, and the safeguards around the quick-opening door. Missing evidence in any of these areas can prevent a defensible release to service, even when production performance appears satisfactory.
Establish which rules govern the installed vessel
The starting point is the location where the autoclave will operate. Pressure vessel requirements differ between countries and can also vary between states, provinces, or other local jurisdictions. The purchaser should establish the accepted construction code, required conformity assessment, registration obligations, and in-service inspection arrangements before finalizing the equipment specification.
Keep construction requirements separate from operating requirements. A construction code addresses matters such as materials, design, fabrication, examination, and testing. In-service rules determine how the vessel is registered, examined, maintained, repaired, and returned to operation. An imported autoclave may have a substantial manufacturing dossier yet still require local acceptance and inspection before use.
How major code frameworks affect the review
ASME Boiler and Pressure Vessel Code Section VIII is a recognized framework for pressure vessel construction. Where an ASME-certified vessel is specified, check the required division, certification scope, nameplate details, and corresponding manufacturer’s data report. An ASME mark does not replace installation permits or periodic inspections required by the operating jurisdiction.
For equipment within the scope of the European Union’s Pressure Equipment Directive, the assessment concerns the applicable essential safety requirements and conformity assessment route. EN 13445 provides a standards route for unfired pressure vessels; it is not interchangeable with the directive itself. Depending on how the equipment is supplied, the conformity assessment may also need to address an assembly of connected pressure equipment.
In China, applicable special equipment legislation, pressure vessel safety technical specifications, and associated standards can govern manufacture, installation, use registration, and periodic inspection. For equipment intended for another market, domestic manufacturing approval alone does not establish acceptance at the destination.
These frameworks should not be treated as equivalent labels. A specification that simply says “ASME/PED compliant” leaves important questions unanswered. Identify the actual construction basis, the legally required assessment route, and the organization responsible for each approval or inspection. Any proposed alternative code needs acceptance through the relevant jurisdictional process.
Match the documentation to the physical equipment
Review the nameplate against the manufacturing dossier and installed configuration. Vessel identification, design pressure, design temperature, volume, materials, and certification details should be consistent. The allowable pressure and temperature must accommodate the intended operating envelope, including credible deviations identified during the safety review.
The handover package should contain the records required by the applicable code and contract. Depending on that basis, these can include material traceability, welding qualifications, examination reports, heat-treatment records, pressure-test results, drawings, and operating instructions. A quality management certificate such as ISO 9001 addresses the manufacturer’s management system; it does not certify an individual autoclave’s pressure integrity.
Inspect the damage mechanisms created by AAC service
AAC curing subjects the autoclave to repeated heating, pressurization, depressurization, and cooling. Inspection planning therefore needs to consider cyclic loading as well as remaining wall thickness. The relevant fatigue assessment depends on the vessel design, number and severity of cycles, operating history, and applicable code requirements. A vessel with acceptable thickness readings may still need investigation for cracking at locally stressed features.
Give particular attention to door assemblies, welds, nozzles, support attachments, and areas where geometry concentrates stress. Door locking components also experience repeated mechanical movement. Misalignment, wear, or uneven engagement can change how loads pass through the closure, even before an obvious leak appears.
Condensate creates another inspection priority. Water retention, poor drainage, and unsuitable water chemistry can contribute to localized corrosion. Low points, drain connections, and locations where deposits accumulate deserve targeted examination. On insulated vessels, external corrosion may remain hidden where moisture enters through damaged weatherproofing or around penetrations.
A useful inspection plan connects each suspected damage mechanism with a suitable examination method:
- Internal and external visual examination: assess corrosion, deposits, distortion, leakage evidence, insulation condition, and accessible closure components.
- Ultrasonic thickness measurement: establish and compare wall thickness at documented locations, with broader scanning where localized loss is suspected.
- Targeted surface or volumetric examination: investigate crack-sensitive locations using methods selected for the material, geometry, and suspected defect.
- Mechanical examination: assess locking elements, hinges, bearings, alignment, and supports against the manufacturer’s acceptance criteria.
A list of thickness readings has limited value without location references, measurement conditions, and an engineering basis for acceptance. Comparing the lowest reading only with nominal plate thickness is insufficient. The assessment must relate the findings to the required thickness, allowable conditions, corrosion allowance where applicable, and measurement uncertainty.
Pressure testing has a specific role, but it does not replace examination for deterioration or cracking. Whether a test is required after installation, repair, alteration, or a particular inspection depends on the governing rules and approved procedure. Pneumatic testing introduces substantial stored-energy hazards and requires specific engineering justification and controls; it should not be selected simply to avoid filling and drying the vessel.
Verify door protection and pressure relief as separate safety functions
The quick-opening door deserves its own verification procedure. A closure failure can release steam and move heavy components violently. Safe operation depends on the condition of the closure, reliable confirmation of engagement, and safeguards that control both steam admission and opening.
The approved arrangement should prevent pressurization when the door is not correctly secured and prevent unsafe opening while pressure remains. The exact sequence and hardware depend on the design. Review the manufacturer’s logic and mechanical safeguards together: a switch showing “closed” may establish door position without proving full locking engagement.
Functional tests should demonstrate the required response to incomplete closure, loss of a relevant signal, and other foreseeable faults identified in the safety assessment. Testing needs a controlled procedure, competent personnel, and protection against unintended steam admission. Routine production operation is not an appropriate way to experiment with interlock failures.
Before opening, the procedure must establish depressurization and address the risk of trapped pressure. An indicated zero on one gauge is weak evidence if the instrument or its connection could be defective. Verify that the designed venting and pressure-confirmation arrangements work, and keep personnel clear of the door’s potential movement path.
Pressure relief devices serve a different purpose from operating controls and door interlocks. Their selection must address credible overpressure scenarios, with set pressure, capacity, installation, and discharge arrangements consistent with the vessel’s allowable limits and governing requirements. Scenarios may include steam control failure or unintended communication with a higher-pressure source.
Inspection should cover the full relief path. A correctly certified valve can still be ineffective if its inlet is obstructed, an isolation valve is incorrectly positioned, or its discharge piping creates unacceptable backpressure. Steam discharge also needs to terminate in a location that manages the hazard to personnel.
Keep operating pressure controls, alarms, shutdown functions, and relief devices distinct in maintenance records. A calibrated pressure transmitter does not demonstrate relief valve performance. Likewise, a relief valve service certificate does not prove that the shutdown logic or door interlock works.
Set inspection timing from legal requirements and condition
There is no single inspection interval suitable for every AAC autoclave system. Mandatory periods depend on the jurisdiction and equipment classification. Within those requirements, inspection planning should account for service severity, deterioration rates, manufacturer instructions, previous findings, and any formally accepted condition-based or risk-based approach.
Separate routine operator checks from examinations performed by competent inspectors or authorized inspection bodies. Operators can identify leakage, unusual noises, drainage problems, abnormal door movement, and damaged indicators. These observations support early intervention, but they do not substitute for the required pressure vessel examination.
A scheduled inspection date should never prevent an earlier assessment when conditions change. Relevant triggers include an overpressure event, significant temperature excursion, repeated door leakage, damaged locking components, suspected cracking, unexpected wall loss, or a modification affecting pressure containment or protective functions. Repairs and alterations may require approved procedures, qualified personnel, additional examination, and jurisdictional authorization.
Production changes also deserve review. When integrating an autoclave into an AAC Block Production Line, changes to batch scheduling, steam recovery, transfer piping, or control sequences can affect cycle frequency and pressure behavior. Shared steam systems require clear equipment boundaries so that isolation, relief protection, and operating responsibility remain defined across connected vessels.
Increasing throughput by shortening heating or cooling stages may change thermal stresses and condensate behavior. Confirm that revised recipes remain within the approved operating envelope and any design assumptions relevant to cyclic service. Maintaining the same maximum pressure does not, by itself, establish that a faster cycle is acceptable.
Keep records that support a release-to-service decision
The most useful inspection file allows a reviewer to connect a finding with an acceptance criterion, corrective action, and authorized decision. A signed checklist saying “satisfactory” is difficult to assess when it lacks examination coverage, measured results, equipment identification, or reference to the governing requirements.
Maintain a controlled record set covering:
- Equipment identity and design basis: nameplate information, drawings, construction records, allowable limits, and applicable registration or acceptance documents.
- Condition history: inspection reports, thickness maps, relevant examination results, defect assessments, repairs, and alterations.
- Protective functions: relief device identification and service records, instrument calibration, interlock tests, and approved control changes.
- Operating exposure: cycle history where required or relevant, excursions, leaks, shutdown events, and changes to steam supply or curing recipes.
- Outstanding actions: responsibilities, completion dates, operating restrictions, and the basis for any continued operation.
For QC and safety personnel, unresolved discrepancies deserve explicit decisions. A mismatched relief setting, undocumented weld repair, or bypassed interlock should have a named owner and a documented disposition before production release. Where examination identifies deterioration, the assessment should state whether operation is acceptable, under what limits, and when further examination is required.
A defensible release to service brings three things together: accepted construction and installation records, current evidence of pressure-boundary condition, and demonstrated operation of protective functions. When one is missing, the next action should address that specific gap. Good curing results and a stable pressure display cannot supply the missing evidence.
Recommend
 Oct 31, 2026
Which Is More Durable: Color Tile or Concrete Roof Tile?
Which is more durable: color tile or concrete roof tile? Compare materials, weather resistance, and manufacturing quality to choose the right roofing with confidence.
- Oct 31, 2026
What Does Hongfa AAC Factory Planning Consulting Include?
Explore what Hongfa AAC factory planning consulting should cover, from raw materials and layouts to utilities and deliverables, to make informed investment decisions.
- Oct 30, 2026
Which Hongfa Hydraulic Brick Machine Specifications Should Buyers Check?
Compare Hongfa hydraulic brick making machine specifications, from forming pressure and output to molds and power demand. Discover what to verify before investing in your production line.