How Accurate Does an AAC Batching System Need to Be?
How Accurate Does an AAC Batching System Need to Be?
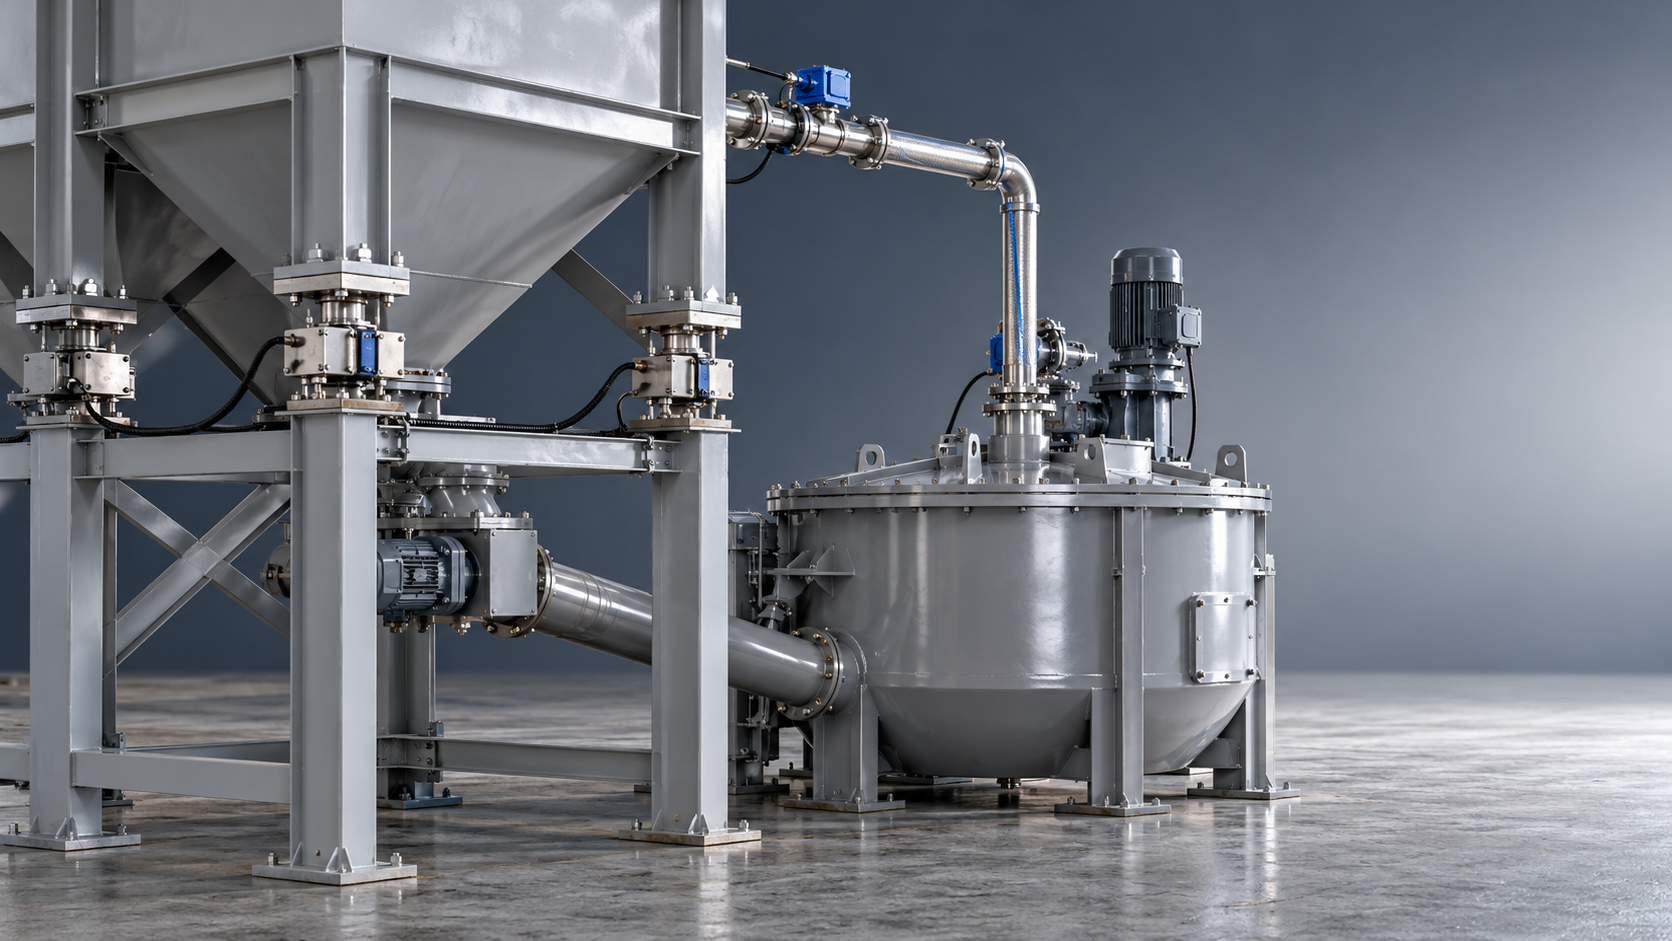
How much dosing error can your AAC production line tolerate before block quality suffers? Whether you choose sand or fly ash, the answer depends on your recipe, raw material variability, and control of critical additions such as aluminum and water. An AAC batching system needs more than precise scales: it must deliver repeatable proportions under actual operating conditions.
There is no single accuracy percentage that guarantees acceptable autoclaved aerated concrete. A useful specification defines accuracy for each material, at its actual batch size, and verifies what reaches the mixer. It must also account for changes in slurry solids, aluminum concentration, and raw material reactivity. Otherwise, a plant can record apparently correct weights while producing inconsistent green cakes.
Start with the recipe’s tolerance, not the scale’s display
The practical question is not “How many decimal places can the controller show?” It is “How far can each ingredient move before the process leaves its validated operating window?” That window should be established through formulation work and production trials using representative raw materials.
Different ingredients create different risks. Variations in cement and lime affect binder balance and reaction behavior. Water changes slurry consistency and the conditions for gas expansion. Aluminum controls gas generation, but its effect also depends on activity, dispersion, temperature, and timing. Siliceous materials contribute both solids and variability in chemical and physical properties.
This makes one blanket tolerance for every dosing circuit difficult to justify. Specify allowable deviations by ingredient and operating range, rather than applying one percentage across the entire AAC batching system. A large slurry scale and a small aluminum dosing unit should not be evaluated as though they perform the same task.
Where recipe sensitivity is not yet established, treat proposed equipment tolerances as provisional. Confirm them during commissioning against casting behavior, cutting readiness, dry density, compressive strength, and the relevant product requirements—not simply against a successful weighing demonstration.
What an accuracy claim actually needs to say
“Accuracy ±0.5%” sounds precise, but it is incomplete unless the reference is stated. Does it mean percentage of target weight, actual reading, or full-scale capacity? Is it a static weighing claim or a guarantee for automatic batching with material flowing through the feeder?
Consider a hypothetical scale with a 2,000 kg capacity, used to weigh a 200 kg addition. A deviation of 0.5% of full scale equals 10 kg, or 5% of that target addition. By contrast, 0.5% of the target equals 1 kg. These figures illustrate the importance of the reference basis; they are not recommended AAC production tolerances.
Three distinctions matter when reviewing quotations:
- Resolution: the smallest increment displayed. A fine display does not establish measurement accuracy.
- Accuracy: how closely the measured or delivered quantity agrees with a suitable reference.
- Repeatability: how consistently the system delivers the same result under comparable conditions.
A repeatable system can still carry a calibration bias. An accurately calibrated scale can still batch inconsistently because of feeder overshoot, vibration, or material sticking. Procurement documents should therefore address both measurement performance and automatic dosing performance.
Sand or fly ash? Control the solids, not just the wet weight
The choice between sand and fly ash changes the material preparation requirements, but neither route eliminates the need to control slurry composition. A slurry scale measures total mass. It does not automatically distinguish useful dry solids from water.
For illustration, a 1,000 kg slurry batch at 60% solids contains 600 kg of dry solids and 400 kg of water. At 58% solids, the same weighed quantity contains 580 kg of solids and 420 kg of water. The scale can be exactly on target while the recipe receives 20 kg less solids and 20 kg more water.
For sand-based AAC, relevant controls include incoming moisture, grinding fineness, slurry solids concentration, and suspension uniformity. For fly ash, source-dependent properties such as fineness, chemical composition, and unburned carbon content can also affect formulation behavior. Equal masses of different fly ash deliveries should not automatically be treated as chemically equivalent.
Where slurry density is used to estimate solids content, validate the relationship for the actual material. Changes in composition or entrained air can make a density reading misleading. Representative sampling, adequate tank agitation, and a documented checking method are as important as the instrument itself.
Returned cutting slurry needs similar attention. Its solids and water enter the next batch and should be included in the material balance. Adjusting fresh water without accounting for return slurry can hide a substantial source of variation.
Give aluminum and water separate control strategies
Aluminum deserves particular attention because its addition is small relative to the total batch, while its effect on expansion is significant. The dosing arrangement should match the actual preparation method, whether the plant uses a prepared suspension, paste-based preparation, or another validated system.
Weighing the carrier liquid accurately is not enough if aluminum concentration varies. Suspension settling, inconsistent preparation, incomplete discharge, and material retained in transfer lines can all change the effective addition. The acceptance check should cover preparation concentration, agitation, dose measurement, transfer, and delivery to the mixer. Aluminum handling also requires appropriate safety measures for the material form and installation.
Water needs a whole-batch calculation. Fresh water is only one contribution; slurry water, return slurry, aluminum preparation water, and rinse water entering the batch may also matter. A controller that accurately meters fresh water but ignores these streams is controlling only part of the recipe.
Temperature should be recorded alongside quantities. Correct proportions do not guarantee consistent rise behavior when incoming slurry temperature or lime reactivity changes. Avoid using aluminum dose adjustments to compensate blindly for every process disturbance.
Why a calibrated system can still miss the batch
Calibration verifies the weighing arrangement under defined conditions. Production adds moving material, pressure changes, mechanical forces, and cycle-time constraints.
Powder continues falling after a screw feeder stops. Liquid continues moving after a valve receives its closing signal. The controller must account for this in-flight material. Coarse and fine feeding, suitable shutoff devices, and tuned cutoff compensation help, but their effectiveness depends on stable material flow.
Mechanical installation can undermine even good instrumentation. Rigid pipe connections may load the weigh vessel. Material buildup can create contact with surrounding structures. Mixer vibration, poorly arranged flexible connections, and unsuitable venting can disturb readings. These faults are not solved by selecting a display with more digits.
There is also a difference between weighing and delivery. Material left in a hopper or transfer line has been measured but has not necessarily reached the mixer. Zero-return checks, discharge confirmation, and inspection of buildup-prone points help reveal that gap. The system should not silently tare away unexplained residue and continue as though nothing happened.
Make acceptance testing resemble production
A useful acceptance plan tests the system across its intended operating range, including smaller recipe additions and normal cycle speeds. A full-load demonstration alone may conceal poor performance at low doses.
- Define each guarantee. State the material, target range, tolerance basis, test method, and operating conditions.
- Check weighing independently. Use suitable reference equipment or calibrated test weights, with measurement uncertainty appropriate to the claimed tolerance.
- Run repeated automatic batches. Review individual deviations as well as averages. Positive and negative errors can cancel in an average.
- Verify transfer and discharge. Check whether the weighed quantity actually reaches the intended destination.
- Challenge normal disturbances. Include relevant hopper levels, replenishment conditions, restarts, and representative material characteristics.
- Confirm exception handling. An out-of-tolerance addition should trigger an agreed hold, correction, or rejection procedure—not disappear into the next process step.
Keep batch records that connect target and actual quantities with raw material lots, slurry measurements, temperatures, and finished-product results. This makes it possible to distinguish a dosing problem from a raw material or curing problem. Without that connection, operators may repeatedly alter a sound recipe to chase unrelated variation.
Specify the process interface, not just the equipment
For a new line or retrofit, clarify who owns slurry compensation, recipe validation, dosing calibration, and commissioning acceptance. Separate suppliers can each meet a narrow equipment specification while leaving gaps between material preparation, batching, mixing, and casting.
Shandong Hongfa Scientific Industrial & Trading Co., Ltd., founded in 1990, manufactures AAC production lines and concrete batching equipment within its construction machinery portfolio. When discussing an integrated project with Hongfa or another line manufacturer, the valuable discussion is how these stages will work together: which material properties the recipe assumes, how changes are measured, and what the controls do when limits are exceeded.
An AAC batching system is accurate enough when it repeatedly delivers the required effective proportions within a validated process window. Before approving a specification, ask for an ingredient-by-ingredient performance schedule and a production-based acceptance plan. Those documents tell you far more than a single impressive accuracy figure.
Recommend
 Oct 26, 2026
Hollow Block Making Machine: Fixing Cracks During Demolding
Hollow block making machine cracks during demolding? Discover how to check mix moisture, compaction, mold friction, and pallet support to reduce waste and improve block quality.
 Oct 26, 2026
How Accurate Does an AAC Batching System Need to Be?
Choosing sand or fly ash? Discover how to specify AAC batching accuracy, control slurry solids and aluminum dosing, and verify performance for consistent block quality.
- Oct 26, 2026
Which Concrete Brick Machine Is Suitable for a Small Factory?
Which concrete brick machine is suitable for a small factory? Compare semi-automatic and automatic options, costs, space, and output to find the right fit for your budget.