How Often Should AAC Molds Be Inspected and Replaced?
AAC mold problems rarely begin with a complete failure. More often, an operator notices that blocks are slightly out of square after cutting, the green cake releases unevenly, slurry residue collects around a joint, or a side panel takes more effort to close than it did before. Left unresolved, these small changes can affect cake geometry, cutting accuracy, surface quality, steam-curing workflow, and unplanned downtime.
AAC molds should be visually checked during every production shift, inspected more closely at least weekly, and measured or condition-assessed at planned maintenance intervals. They should be replaced not simply because they reach a fixed age, but when deformation, cracking, corrosion loss, damaged sealing surfaces, worn locking points, or repeated quality issues can no longer be corrected safely and economically. The exact interval depends on mold design, production volume, handling method, slurry formulation, cleaning practice, and the severity of the thermal cycle.
Use several inspection intervals instead of one replacement date
A mold used in an autoclaved aerated concrete line is exposed to wet slurry, alkaline materials, repeated heating and cooling, vibration, lifting loads, demolding forces, and cleaning operations. A calendar-only rule may miss a rapidly developing defect, while replacing molds strictly by age can discard components that remain structurally sound.
A more reliable approach separates routine observations from planned technical inspections. The production team can identify immediate operating changes, while maintenance personnel verify alignment, structural condition, and wear trends before those changes affect the line.
The planned intervals should be shortened when production is intensive, molds are cleaned aggressively, or the plant has recurring problems with leakage, sticking, or cake deformation. Conversely, a lightly used standby mold still needs inspection before returning to operation because corrosion, seized hardware, or degraded seals can develop while it is stored.
What operators should notice during normal production
The fastest inspection is not a formal measurement. It is the practical observation made when a mold is prepared, filled, opened, cleaned, and returned to the cycle. These checks take little time when they are built into normal handling.
- Look for slurry weeping from joints, corners, bottom interfaces, or around closure points during filling and pre-curing.
- Check whether side panels close evenly and whether locks engage without excessive force, improvised leverage, or repeated adjustment.
- Watch for hardened AAC residue along sealing faces, hinges, and the bottom edge of the mold.
- Observe whether the green cake separates consistently during demolding or begins to drag, tear, or remain attached to one surface.
- Check that lifting lugs, trunnions, brackets, and attachment points show no cracks, elongation, looseness, or fresh distortion.
- Notice changes in the finished cake before cutting, especially bowed sides, uneven height, corner defects, or a persistent out-of-square shape.
One imperfect cake does not automatically prove that the mold is defective. Mixing consistency, filling level, expansion behavior, pre-curing conditions, release agent application, and handling can also cause defects. However, when the same problem follows one mold through several cycles, that mold should be isolated for inspection rather than repeatedly adjusted on the production floor.
Signs that a mold needs repair, refurbishment, or replacement
The question is not always whether the mold is “good” or “bad.” Some conditions can be repaired through cleaning, seal replacement, hinge adjustment, local welding, surface restoration, or frame correction. Others indicate that continued use creates a quality or safety risk.
Usually repairable conditions
Replaceable seals that have flattened, hardened, torn, or lost elasticity are a normal maintenance item. Surface residue, light corrosion, worn release coating, loose fasteners, and minor hinge wear can also be addressed if the underlying structure remains stable. A side panel that does not seat correctly may be caused by debris in the joint, a worn pin, or a maladjusted lock rather than permanent distortion.
Minor weld damage should not be ignored simply because the mold still operates. A qualified repair assessment should determine whether the crack is superficial or related to a load-bearing area. After repair, the mold must be checked for alignment and safe lifting condition, not merely returned to production because the visible crack has been covered.
Conditions that often justify removal from service
Replacement becomes the practical choice when a mold no longer holds its intended geometry or when repairs would be frequent, uncertain, or likely to affect its rigidity. Important warning signs include:
- Permanent warping of the base, frame, or side panels that prevents repeatable closure.
- Cracks in structural members, lifting points, major welds, or load-bearing corners.
- Repeated slurry leakage after seals, seating faces, and locking mechanisms have been serviced.
- Excessive corrosion that reduces section thickness or damages critical contact surfaces.
- Elongated holes, badly worn hinge locations, or lock points that cannot hold the mold closed consistently.
- Persistent dimensional errors in the green cake that are traced to the same mold.
- Repairs that require repeated heating, straightening, welding, or re-machining without restoring stable performance.
A mold with damaged lifting features deserves immediate attention. Even if the mold produces acceptable cakes, lifting equipment transfers significant loads through these points. Any suspected defect in lugs, hooks, trunnions, or their weld areas should be evaluated before the mold is moved again.
Measure geometry when quality symptoms point to the mold
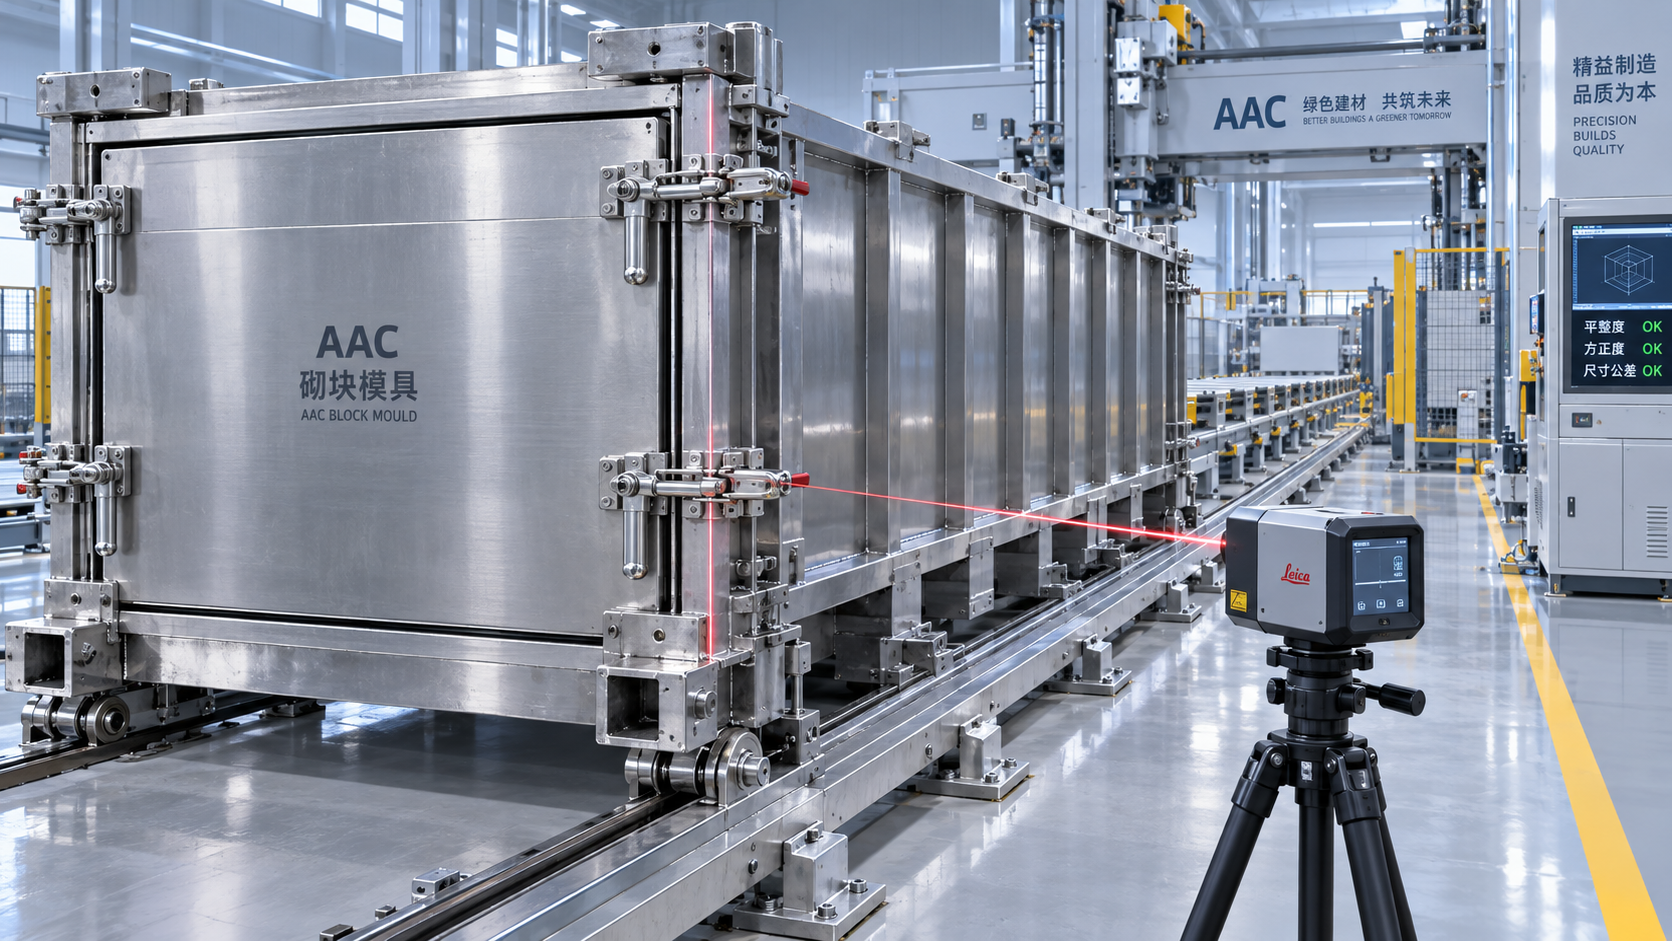
Visual inspection can reveal major damage, but it cannot confirm whether the mold remains within the dimensional limits needed for accurate cutting. When block size variation, poor squareness, uneven cake height, or recurring side damage appears, maintenance should measure the mold according to its design drawings or approved tolerances.
The inspection should generally compare opposite side lengths, diagonal dimensions, panel straightness, base flatness, corner squareness, and the relationship between side panels and the base. Closure should be checked with the mold clean and with its normal locks engaged. Measurements taken over hardened residue or with panels only partly seated can lead to a false diagnosis.
Documenting results by mold identification is more useful than maintaining a vague note that “molds were checked.” A simple record can show whether one mold is drifting over time, whether a repair restored stability, and whether a recurring product defect is actually linked to a particular tool. It also helps separate normal seal wear from structural deterioration.
Why leakage should never be treated as only a housekeeping issue
Slurry leakage around a mold joint creates more than cleanup work. It may reduce the intended cake profile, build hardened material on critical surfaces, interfere with closure, and gradually force operators to compensate with extra clamping or improvised adjustments. Those responses can hide the original problem while placing more stress on locks and hinges.
Start by identifying the exact leak path. Check for residue on the mating faces, damaged or incorrectly seated seals, uneven panel contact, bent edges, loose fasteners, and insufficient locking force. A leak concentrated near one corner may suggest a local seating problem. Leakage along a long section can indicate a worn seal, a distorted panel, or an issue with the base interface.
Do not compensate for a leaking mold by overapplying release agent or overtightening mechanisms beyond their intended operation. Excessive release agent can affect surface conditions, while excessive clamping force may accelerate wear or damage the mold frame. The correction should restore proper contact and alignment.
Cleaning methods influence inspection frequency
AAC residue becomes harder to remove as it cures. Delayed cleaning can lead to scraping, striking, or forceful mechanical removal that damages sealing faces and thin edges. Over time, even minor nicks on the closing surface can create leak paths.
Cleaning should remove residue before it interferes with mold closure, but tools and methods need to match the surface. Avoid uncontrolled hammering, deep gouging, and abrasive techniques that alter critical contact faces. After cleaning, inspect the areas that were covered by buildup; corrosion and cracking often remain hidden until residue is removed.
Release agent should be applied evenly and only where specified by the process. Too little can contribute to sticking, but excessive material can attract dust and slurry residue, obscure defects, and complicate later cleaning. When demolding becomes inconsistent, inspect both the release practice and the mold surface before concluding that the mold must be replaced.
Build replacement decisions around condition and downtime risk
A replacement plan should consider more than the purchase cost of a new mold. A mold that repeatedly requires adjustment may consume labor, interrupt cycle timing, increase reject risk, and create uncertainty in production planning. On the other hand, replacing a mold with a minor serviceable defect may not be justified if alignment, structural integrity, and sealing performance can be restored.
It is useful to classify molds into three internal conditions: fit for normal operation, fit for operation after scheduled repair, and removed from service pending technical evaluation. This prevents a borderline mold from circulating indefinitely because no one has made a clear disposition decision.
Keep spare seals, pins, fasteners, and other normal wear components available for the specific mold design. For major structural components, use compatible parts and repair methods that preserve the mold’s original geometry. When a repair changes a structural member or a lifting area, confirm the work against the equipment documentation and applicable site safety procedures.
Frequently asked questions
Can AAC molds be inspected only during annual maintenance?
No. Annual or major shutdown inspections are useful for detailed measurements and structural work, but they are too infrequent for issues such as seal damage, residue buildup, loose hardware, leakage, and developing cracks. Shift-level observation and routine weekly checks are needed to catch operating problems early.
How do we know whether poor block dimensions come from the mold or the cutting system?
Compare the green cake before it reaches cutting with the final cut product. If the cake is already bowed, uneven, or out of square, inspect the mold, filling process, and pre-curing conditions. If the cake is consistent but finished dimensions vary, examine wire condition, cutting alignment, machine settings, and cake positioning.
Should a mold be replaced after any weld repair?
Not necessarily. The decision depends on the repair location, the extent of damage, the load carried by that area, and whether geometry can be verified afterward. A minor non-structural repair is different from cracking at a lifting point, frame corner, or heavily loaded joint. Structural repairs should be assessed before the mold returns to service.
Next:No more content
Recommend
 Oct 11, 2026
How Often Should AAC Molds Be Inspected and Replaced?
How often should AAC molds be inspected and replaced? Discover practical inspection schedules, warning signs, and maintenance tips to reduce defects and downtime.
- Oct 10, 2026
What Safety Standards Apply to AAC Autoclave Systems in Europe?
What safety standards apply to AAC autoclave systems in Europe? Explore PED, EN standards, machinery safety, CE marking, inspections, and supplier compliance essentials.
 Oct 11, 2026
What to assess before selecting an AAC mixing and pouring system
AAC Mixing and Pouring System selection guide: assess batching accuracy, slurry consistency, automation and reliability for stable AAC production.