Which concrete block production line fits your planned output capacity
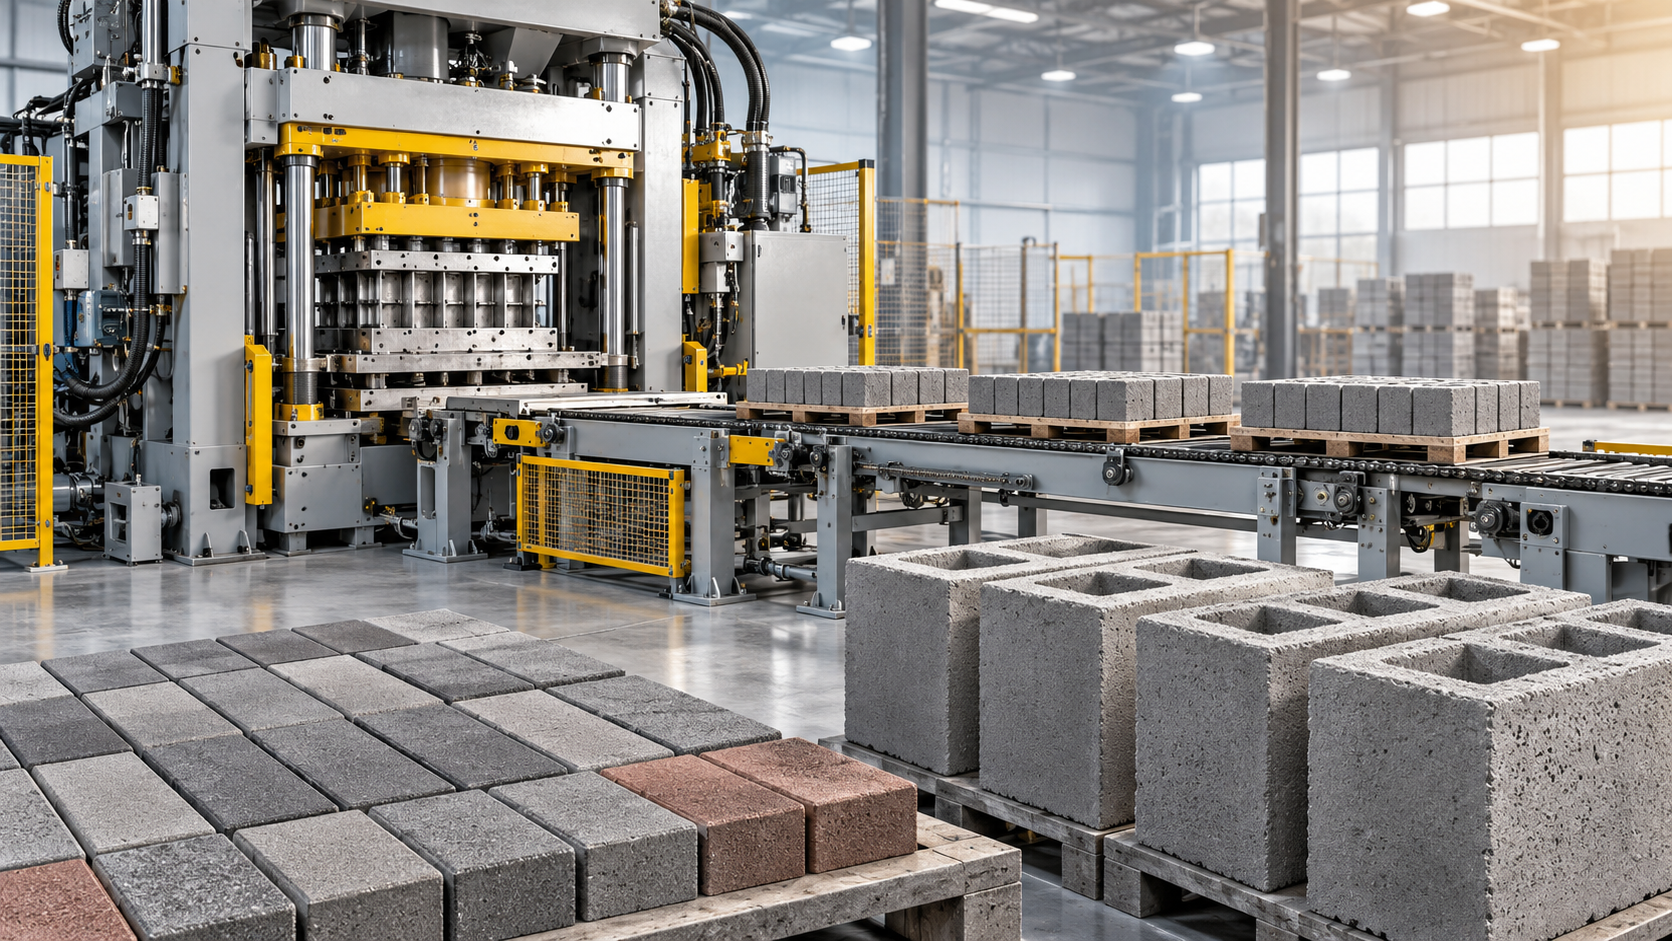
Start with the output that must leave the yard as saleable blocks, not the theoretical capacity printed for a single machine. A concrete block production line is a chain: aggregate handling, batching, mixing, block forming, transfer, curing, and finished-product handling. The line fits the planned capacity only when every stage can sustain the required daily volume without forcing the block machine to wait or allowing green blocks to accumulate before curing.
Capacity should therefore be expressed in the products that will actually be sold: block dimensions, wall thickness, hollow ratio, strength class, and daily production schedule. A line rated by pieces per cycle can look highly productive while producing far less wall area or concrete volume than another model with a different mould layout. Compare output in square metres of wall, cubic metres of finished blocks, or the exact block count required by the sales mix. Then include the expected proportion of each block type rather than calculating from one favourable standard unit.
Begin with the required net daily output
Planned output is often stated as a daily target, while equipment data are stated per moulding cycle or per hour. The conversion between them needs realistic operating assumptions. A shift includes raw-material replenishment, mould changes, routine cleaning, minor adjustments, pallet circulation delays, rejected green blocks, and scheduled maintenance. These are part of normal production rather than exceptional events.
First determine the quantity of acceptable finished blocks needed each working day. Then divide by the planned operating hours, allowing time for activities that do not create blocks. The result is the net hourly requirement. A line should have enough practical output margin to achieve that figure during normal running, rather than only under ideal conditions with one mould and uninterrupted material supply.
For example, a project centered on one common hollow block size has a different capacity profile from a project that alternates among hollow blocks, solid blocks, pavers, kerbs, and specialty units. Smaller products can raise the number of pieces per cycle but may increase stacking, sorting, and handling work. Heavy solid units consume more concrete per pallet position and may constrain curing and transport before the press reaches its nominal moulding limit.
Use cycle time as a system value
The forming cycle includes feeding the mould, vibration, compaction, mould stripping, and transfer to the next pallet. Its duration changes with mix consistency, block geometry, compaction demand, and the condition of the mould and vibration system. A quoted short cycle is useful only if the mixer can deliver homogeneous concrete at the same rhythm and the downstream conveyor has an available pallet at the discharge point.
Calculate capacity from the expected cycle time for the most important products, not from the fastest product in a catalogue. Where several products will be made, calculate each one separately and combine the results according to the expected production ratio. This reveals whether the planned range requires a higher-capacity press, additional mould sets, more curing positions, or simply a better production schedule.
The block machine is not the whole production line
A press can be oversized while the rest of the line remains undersized. The resulting plant will still miss its output target, but the cause may be mistaken for a machine problem. Capacity matching should follow the material flow from incoming aggregate to finished packages.
The mixer deserves close attention because it determines both throughput and block consistency. A larger mixer is not automatically better if its batch size does not align with the concrete demand of the press. Excess concrete can sit and lose its intended moisture condition; too little concrete forces repeated press stops. The target is a batching and mixing rhythm that supplies the hopper steadily, while retaining enough adjustment control for changes in aggregate moisture.
Material moisture is especially influential in semi-dry concrete. A mixture that is only slightly wetter can feed and compact differently, affecting block height, edge definition, stripping stability, and green strength. A line with automatic weighing but weak moisture control may deliver inconsistent output. When local sand, stone dust, recycled aggregate, or cementitious materials vary across deliveries, storage separation and moisture measurement can matter as much as the rated output of the main press.
Match the automation level to volume and product variability
Manual handling can be workable at lower, stable output levels where product changes are limited and space is available for orderly pallet movement. As planned volume rises, repeated manual transfer introduces delays that are difficult to see in a nominal capacity calculation. It also increases the chance of fresh-block damage, inconsistent stacking, and congestion around the curing area.
Semi-automatic arrangements often suit operations that need reliable batching and forming but retain manual control over selected handling or packaging tasks. This layout can be practical when product changeovers are frequent, provided access around the mould, pallet route, and transfer equipment remains clear. The time required to replace a mould and reset feed settings should be included in the production plan; it should not be treated as lost time outside capacity planning.
Higher automation becomes more relevant when continuous output, multi-shift operation, or dense curing systems are planned. Conveyor logic, pallet circulation, automatic cubing, and controlled curing can reduce routine handling constraints, but they also increase the need for coordinated maintenance and accurate commissioning. An automated line that is difficult to access for cleaning or mould replacement can lose more practical capacity than a simpler line designed around the actual product schedule.
Curing capacity often sets the real ceiling
Freshly formed blocks require protected curing conditions and sufficient residence time before handling, stacking, or dispatch. The curing method affects the floor area, rack configuration, pallet quantity, energy demand, and transport arrangement needed to support a given daily output. A forming section that produces more pallets than the curing system can accept will create a bottleneck immediately, even if all upstream equipment is correctly sized.
Estimate the number of pallets produced during each operating period and multiply it by the required curing residence period. Add practical allowance for pallet return, product segregation, and the fact that curing rooms or racks are not always loaded and unloaded in a perfectly continuous pattern. Dense rack systems use space efficiently but depend on dependable transfer equipment and a clear route for removing cured product. Open-yard curing needs more area and is more exposed to weather-related variation.
Curing is also linked to product quality. If blocks are moved before their green strength is adequate, chipped corners, cracked webs, and distorted faces can rise even though the press is producing at the planned rate. Increasing vibration or cement content to compensate for poor handling is rarely a sound capacity solution. The better response is to align stripping strength, transfer timing, and curing availability.
Choose capacity around the dominant product, then test the exceptions
The dominant product should set the core line configuration because it consumes most production time and determines the usual mould, pallet, and curing pattern. However, the exceptions reveal whether the configuration is genuinely flexible. Ask how a change from hollow masonry units to solid blocks affects concrete demand, press settings, cycle time, pallet loading, and curing space. Ask whether pavers or kerbs require different face-mix arrangements, pigment handling, surface control, or secondary handling equipment.
Mould geometry influences more than output count. Thin webs, deep cores, narrow partitions, and detailed surface patterns place different demands on filling and compaction. A mould that produces many units per cycle may not be appropriate for a high-strength product with demanding geometry. The relevant question is whether the press can repeatedly fill and compact that mould with the intended mix, then strip cleanly without damaging the green product.
Confirm the mould mounting interface, pallet dimensions, and support requirements before treating multiple products as interchangeable options. A broad product range may require additional mould storage, lifting arrangements, setup time, and trained adjustment procedures. These supporting needs can affect the usable output more than the mould count itself.
Allow for expansion without buying unused complexity
An expansion plan is meaningful when it identifies the specific constraint likely to change: more working hours, a second mould, higher daily demand, a larger curing zone, or a separate product family. Each expansion path calls for a different initial investment. Selecting a press with reserve forming capacity makes sense only when the batching plant, material storage, pallet inventory, electrical supply, curing space, and dispatch route can be expanded with it.
A modular approach is often appropriate where demand is uncertain. The initial layout can reserve space and interfaces for additional aggregate bins, a larger curing arrangement, extra pallet circulation, or a downstream cubing unit. The present line remains matched to current demand, while later additions do not require rebuilding the entire material route.
Conversely, installing advanced automation for a low and irregular output schedule can create avoidable maintenance exposure. Sensors, conveyors, hydraulic components, vibration assemblies, and control systems require access, spare parts, calibration, and planned inspection. The most productive configuration is the one that can be kept in stable operation with the available maintenance capability.
Compare proposals on a common operating basis
Before selecting a Concrete Block Production Line, request each proposal in the same format: product size and mould cavities, estimated cycle time for that product, batches per hour, mixer discharge volume, pallet size and quantity, curing residence assumption, handling route, installed utilities, and items excluded from the scope. A capacity figure without its product, cycle, and curing assumptions cannot be compared reliably.
Pay attention to boundaries between packages. Equipment suppliers may define the line differently: one quotation may include batching, conveyors, pallets, curing racks, cubing, and control integration, while another may focus on the forming machine. Site civil works, foundations, drainage, dust collection, electrical distribution, compressed air, water supply, and commissioning access also affect whether the planned output is achievable after installation.
A practical selection leaves room for routine variation without relying on constant maximum-speed operation. When material flow, mould performance, curing capacity, and handling are balanced around the actual product mix, the line is more likely to deliver consistent blocks at the output level the operation was planned to support.
Recommend
 Oct 14, 2026
What Is the Difference Between a Concrete Brick Machine and a Block Machine?
What is the difference between concrete brick machine and block machine? Compare products, molds, output, and find the right solution for your plant.
- Oct 13, 2026
How to Choose a Wall Panel Production Machine for Export Quality?
How to choose a wall panel production machine for export quality? Explore essential factors for consistent output, curing, automation, quality control, and supplier support.
- Oct 12, 2026
Is ISO Certification Mandatory for AAC Block Manufacturing Equipment?
Are AAC block manufacturing equipment ISO certified mandatory? Discover legal requirements, supplier risks, and smart compliance checks before investing.