What Should AAC Plant Commissioning Include?
AAC plant commissioning should demonstrate that the complete production line can safely and repeatedly turn the agreed raw materials into saleable autoclaved aerated concrete products. Equipment rotation checks and a successful first batch are necessary milestones, but they do not establish production readiness.
The commissioning scope should cover mechanical and electrical verification, utility readiness, batching calibration, process trials, cutting performance, autoclave safety and curing control, finished-product testing, and operating handover. Acceptance should depend on documented results under defined conditions—not simply on whether the machinery runs.
Define acceptance before production trials begin
A commissioning plan needs a clear distinction between installation completion, permission to operate, process stabilization, and performance acceptance. Combining these into a single “commissioning completed” certificate can leave unresolved quality or safety issues hidden behind an apparently finished project.
Before testing starts, the equipment supplier and plant owner should agree on:
- The products to be demonstrated, including dimensions, density classes, and required strength.
- The raw material specifications and permitted variations during testing.
- The utilities available at the plant boundary, including steam conditions, electrical supply, water, and compressed air.
- The measurement methods, sampling arrangements, and test duration.
- The responsibilities for adjustments, laboratory testing, consumables, and retesting.
- The defects that prevent operation or acceptance, and how outstanding work will be closed.
Capacity also needs an explicit definition. Mixer output, green-cake volume, autoclave throughput, and saleable finished-product volume are not interchangeable. A line can achieve its nominal casting rate while losing substantial output through cutting damage, curing defects, or rejected blocks. Performance acceptance should identify which output is guaranteed and how downtime and rejects are counted.
Verify that the installed plant is ready for controlled operation
Mechanical completion checks should follow the material flow, from receiving and preparation through batching, casting, cutting, autoclaving, and finished-product handling. The objective is to identify conditions that could cause injury, equipment damage, contamination, or unstable processing before materials enter the line.
Checks should include equipment alignment, foundation and fastening condition, lubrication, pipe supports, conveyor tracking, mold condition, transfer-car positioning, and access for inspection and maintenance. Cutting equipment requires particular attention to wire alignment, tensioning arrangements, and the relationship between cake positioning and finished dimensions.
Electrical verification should establish correct motor rotation, instrument identification, grounding, protective functions, and communication between field devices and the control system. Emergency stops, guards, permissives, and interlocks must be functionally tested rather than accepted from drawings alone. Tests should follow approved procedures and be performed by competent personnel.
Utility performance must be verified under representative demand. Adequate pressure at an idle steam header does not demonstrate that the system can supply an autoclave cycle while other users are operating. Similar limitations apply to compressed-air capacity, water delivery, condensate removal, and electrical loading.
Dust collection, drainage, slurry-return systems, and housekeeping provisions also belong in commissioning. Their failure can interrupt production even when the main process machines function correctly.
How accurate must an AAC batching system be?
There is no single batching tolerance that can be applied responsibly to every AAC plant. The required accuracy depends on the recipe, ingredient quantity, material behavior, dosing equipment, and demonstrated sensitivity of the product. Acceptance limits should distinguish major mineral ingredients, water, and small additions such as aluminum-based aerating agent.
A percentage tolerance without a defined reference is incomplete. It must state whether the percentage refers to the target batch quantity, the instrument’s full-scale capacity, or another basis. A scale specification expressed as a percentage of full scale can be unsuitable for a small ingredient dose even when it appears precise.
Commissioning must also separate instrument calibration from actual dosing performance:
Dynamic dosing tests should use the actual materials wherever practicable and cover the intended operating range. Feeder cutoff delay, material remaining in flight, valve leakage, bridging, and vibration can produce errors that are absent during static calibration. Flexible connections and attached pipework must not impose forces that distort weighing.
For slurry ingredients, accurate wet mass is only part of the requirement. If solids concentration changes, an unchanged slurry weight delivers a different amount of mineral solids and water. Recycled slurry adds another variable because its concentration and condition can change with production activity. The recipe-control method must account for these changes using validated measurements.
Small aerating-agent additions require special attention to usable weighing range, preparation consistency, suspension behavior, and complete transfer. Correctly weighing a suspension does not guarantee that the intended active quantity reaches the mixer if settling or residue occurs.
The practical acceptance criterion is therefore a combination of calibrated measurement, repeatable delivery, controlled ingredient condition, and stable product results. Supplier-stated accuracy should be verified at the plant’s actual batch sizes, not accepted solely from an instrument datasheet.
Establish a workable process window before increasing output
AAC commissioning is partly equipment verification and partly process development within the agreed raw material envelope. Sand or fly ash characteristics, lime reactivity, cement properties, sulfate balance, water temperature, and recycled slurry condition can all affect expansion and early strength development.
Baseline testing should characterize the properties relevant to the selected process. For a sand-based route, grinding and slurry preparation need verification against the required fineness and concentration. Where fly ash is used, its relevant physical and chemical variation must be considered. Lime suitability cannot be judged by delivered weight alone; its reaction behavior influences process timing and temperature.
During casting trials, records should link each batch to ingredient quantities, slurry condition, mixing sequence, mixing time, discharge temperature, mold identification, and observed rise behavior. This makes it possible to distinguish a batching problem from a raw material or temperature-control problem.
Pre-curing should produce a cake strong enough for demolding and cutting without excessive deformation, tearing, or collapse. A fixed waiting time is not sufficient evidence of readiness because temperature and material reactivity influence strength development. The plant needs a defined, repeatable method for judging cutting readiness, supported by trial results.
Changing several recipe and process variables simultaneously makes troubleshooting difficult. Controlled adjustments, with a record of the reason and result, provide a more reliable basis for establishing the operating window.
Test cutting, transfers, and recycling as one connected operation
Cutting acceptance should examine the whole cake and finished-product geometry, not only a few undamaged pieces. Relevant checks include dimensional consistency, squareness, surface condition, edge damage, wire drag, and defects introduced during turning or transfer.
A dimensional problem may originate upstream. Uneven cake firmness, mold distortion, poor positioning, or unsuitable pre-curing conditions can resemble a cutting-machine fault. Commissioning records should allow defects to be traced back to the cake and batch rather than attributed automatically to wire settings.
Transfer equipment must demonstrate reliable movement at the intended production rhythm. A line that works only with frequent manual intervention has not demonstrated the same operating capability as a coordinated automatic line.
Cutting-waste recovery should also be operating during representative trials. Recycling changes the water and solids balance; excluding it can make initial trials look stable while leaving the normal production recipe unproven.
Keep autoclave safety approval separate from curing optimization
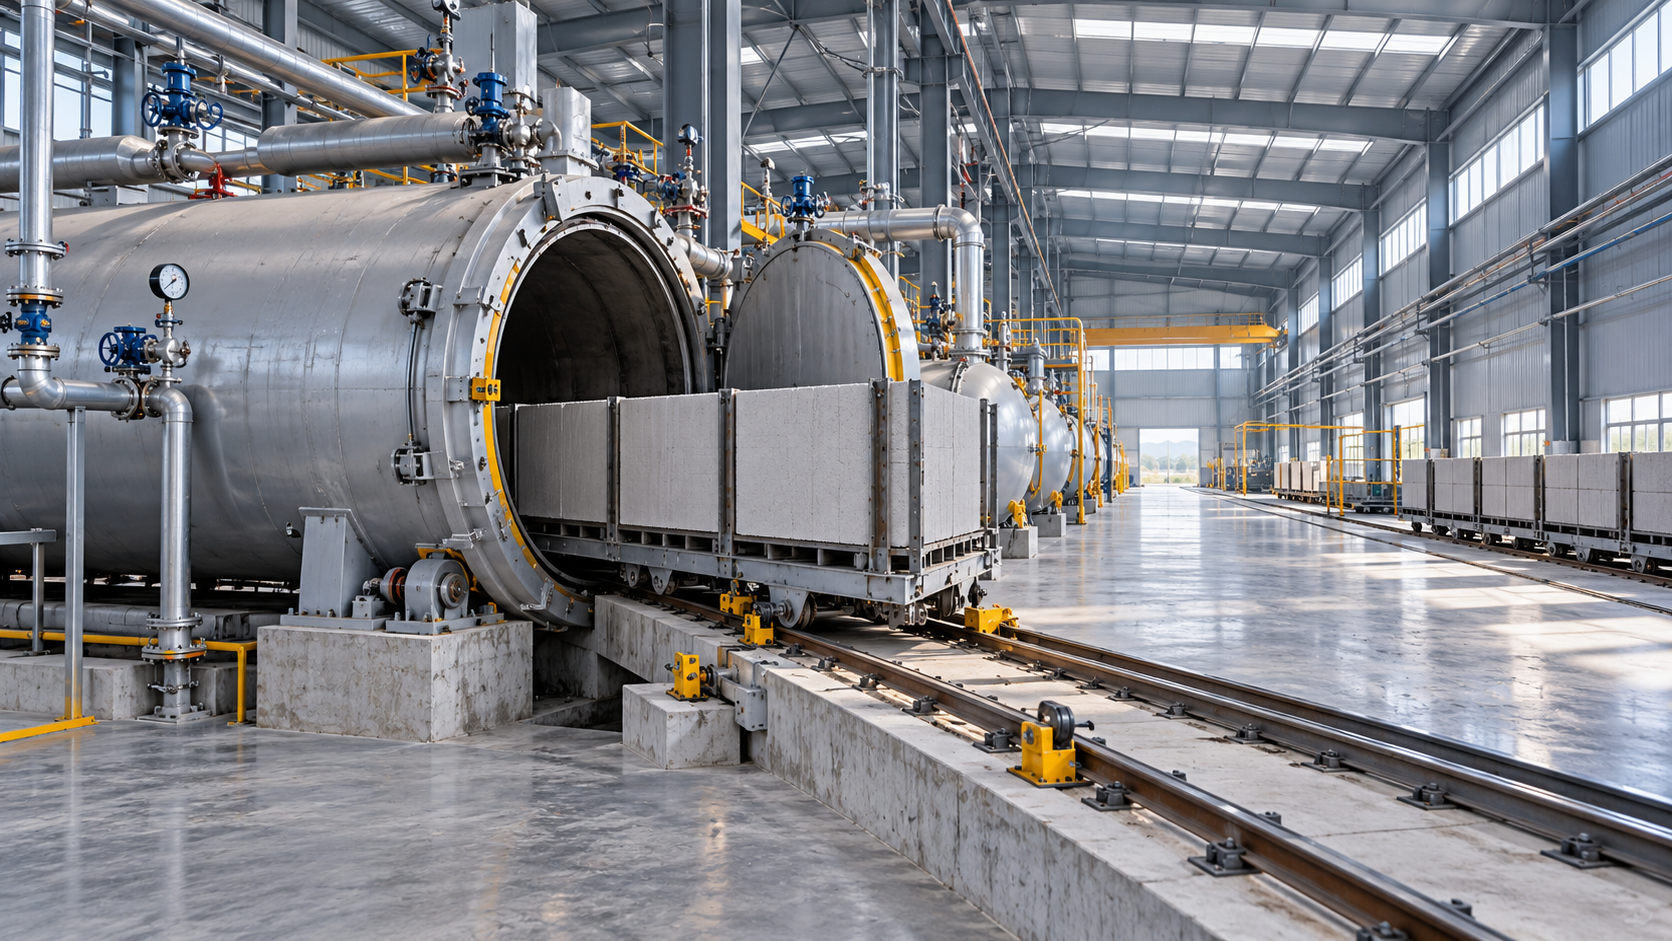
An autoclave is a pressure system, and successful product curing does not prove that it is safe or legally ready for service. Required inspections, pressure-system documentation, protective devices, operating authorization, and personnel competence must satisfy the rules applicable at the installation location.
Commissioning should verify door-locking and pressure-related interlocks, safety-device documentation, instrumentation, steam and condensate arrangements, and the approved operating procedures. Safety-critical checks must follow the vessel manufacturer’s requirements and applicable statutory procedures. Schedule pressure is not a justification for bypassing protective functions.
Process trials should then establish that the curing cycle is suitable for the product and actual loading arrangement. Recorded pressure and temperature profiles, air-removal provisions, condensate behavior, and load distribution help assess whether the specified curing conditions are achieved consistently.
A controller reaching its setpoint does not by itself demonstrate uniform treatment throughout the load. Product sampling should cover relevant positions within the autoclave, particularly where trial results suggest differences. Steam supply and any steam-transfer arrangements should also be tested under the intended production sequence.
Prove quality and throughput over representative operation
One acceptable cake or one successful autoclave load demonstrates feasibility, not repeatability. Performance testing should cover an agreed run long enough to expose interactions among batching, pre-curing, cutting, autoclaving, and handling. Its duration should reflect the process and contractual obligations rather than an arbitrary universal number.
Finished-product testing should use the applicable product standard and agreed laboratory methods. Depending on the product and specification, acceptance may include dry density, compressive strength, dimensions, and other required properties. Test age, moisture condition, specimen preparation, and sampling location must be defined because they affect result comparability.
Density and strength should be evaluated together. Meeting strength by producing materially denser blocks does not demonstrate compliance with a lower-density product specification.
The performance record should reconcile cast volume, cured output, saleable output, rejects, downtime, and rework. If energy or water consumption is guaranteed, the measurement boundary must identify included equipment, startup consumption, steam conditions, and the output basis. Results from partial-load trials should not be presented as proven full-capacity performance.
Hand over a plant that can be operated without the commissioning team
Training should include routine operation, startup and shutdown, abnormal conditions, recipe authorization, sampling, maintenance, and safety responsibilities. Competence is better demonstrated through supervised tasks and responses to defined scenarios than through attendance records alone.
The handover package should contain as-built drawings, equipment manuals, calibration records, safety-test results, approved recipes and operating ranges, laboratory methods, maintenance schedules, spare-parts information, and control-system backups. Software access rights and responsibility for future changes should be clear.
Outstanding items should be recorded with their operational significance, responsible party, and closure requirements. Safety-critical defects must not be treated as ordinary punch-list work. Conditional acceptance, where permitted, should state exactly which performance obligations remain open.
A defensible commissioning sign-off rests on traceable evidence: the installed plant is safe to operate, the process works with the agreed materials, the finished product meets its specification, and the required output is repeatable. That evidence—not a startup ceremony or a single good batch—is what makes an AAC plant ready for production.
Recommend
 Oct 27, 2026
How a Concrete Brick Machine Works—and Why Curing Still Matters
Learn how a concrete brick machine shapes and compacts bricks, why curing builds lasting strength, and which production checks help you choose equipment for reliable, saleable output.
- Oct 26, 2026
Hollow Block Making Machine: Fixing Cracks During Demolding
Hollow block making machine cracks during demolding? Discover how to check mix moisture, compaction, mold friction, and pallet support to reduce waste and improve block quality.
 Oct 27, 2026
How Long Does AAC Plant Installation Usually Take?
What does AAC plant commissioning include? Explore installation timelines, safety checks, material trials, and acceptance milestones to plan a smoother startup and avoid costly delays.